Advanced Industrial Ultrafiltration (UF) Water Treatment Systems
Engineered for High Efficiency, Robust Performance, and Targeted Contaminant Removal in Industrial Applications.
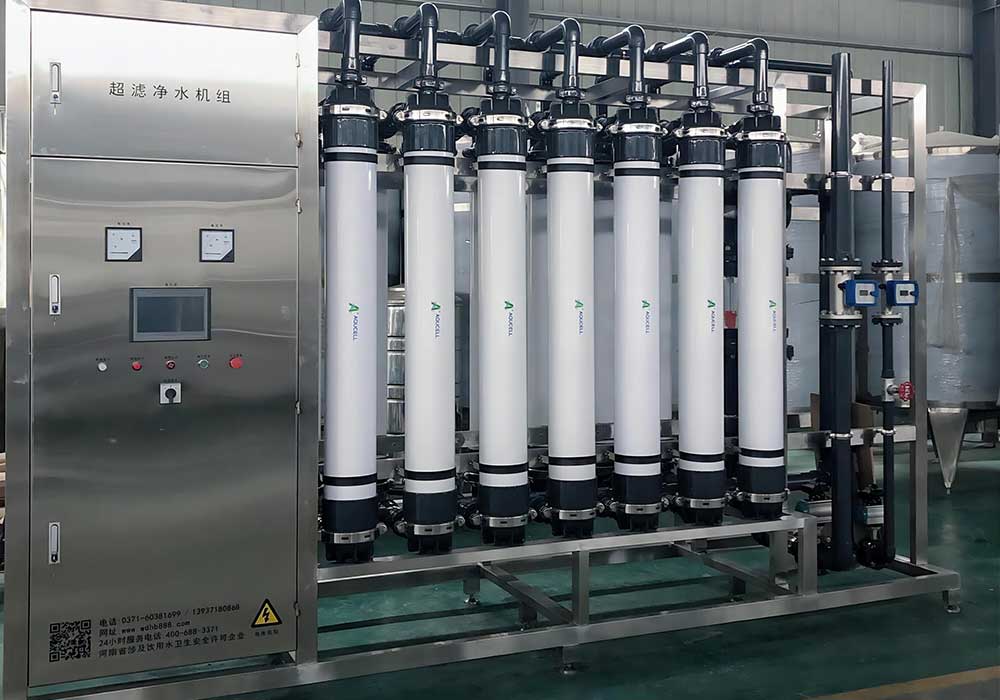
Ultrafiltration System
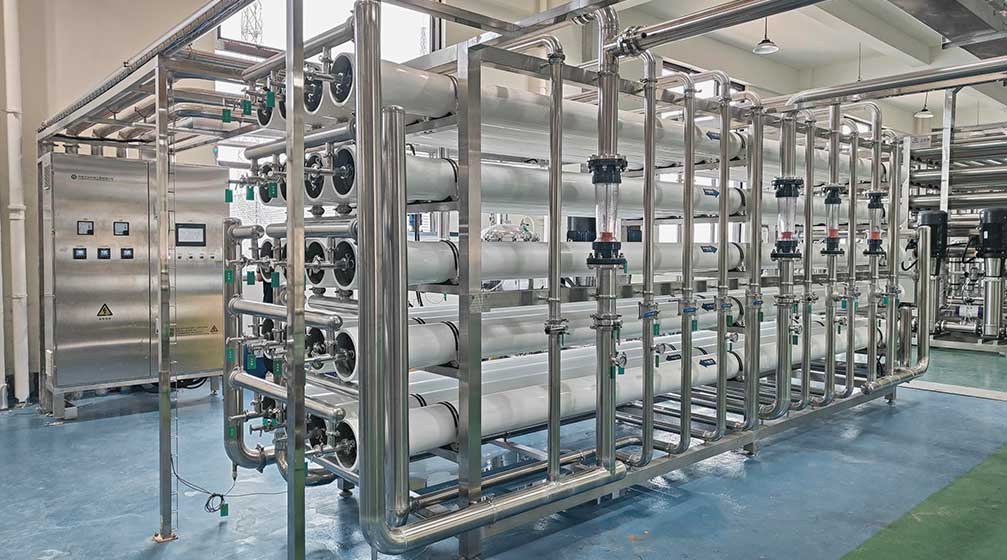
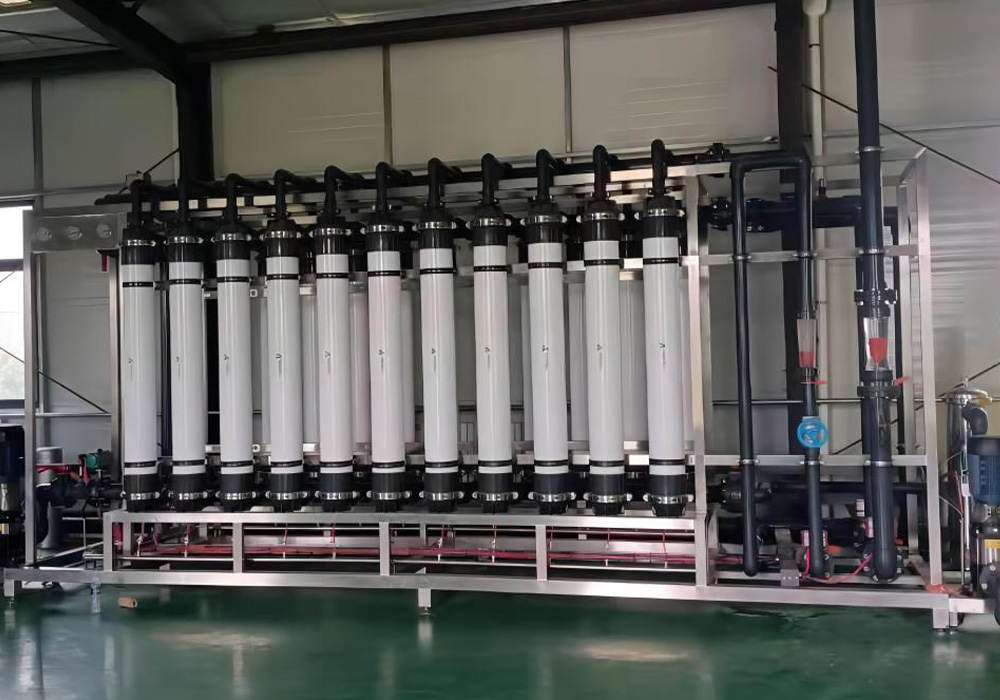
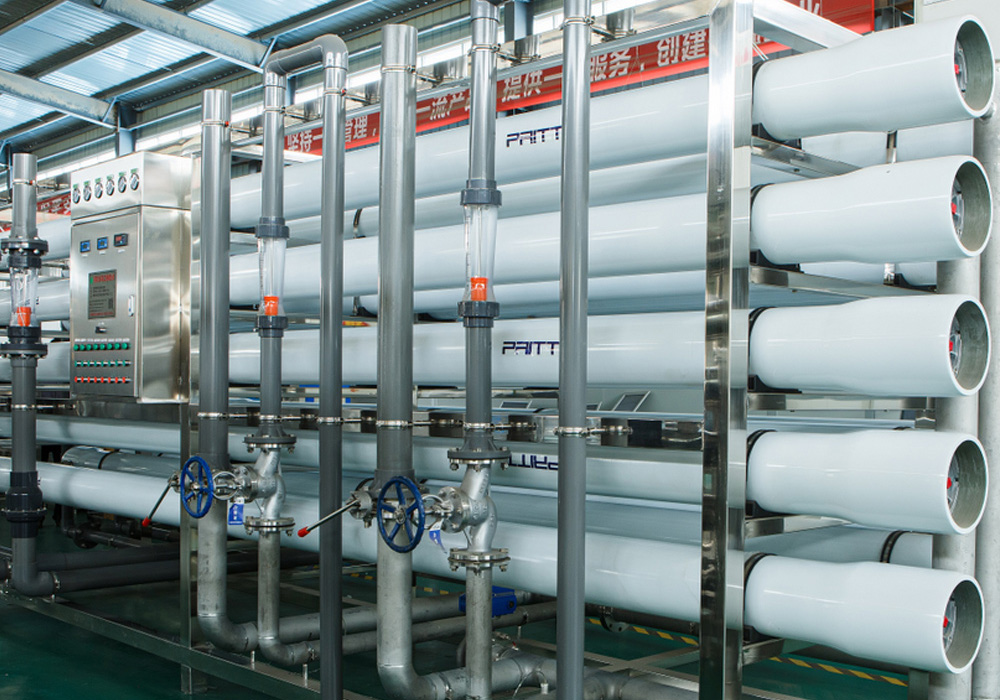
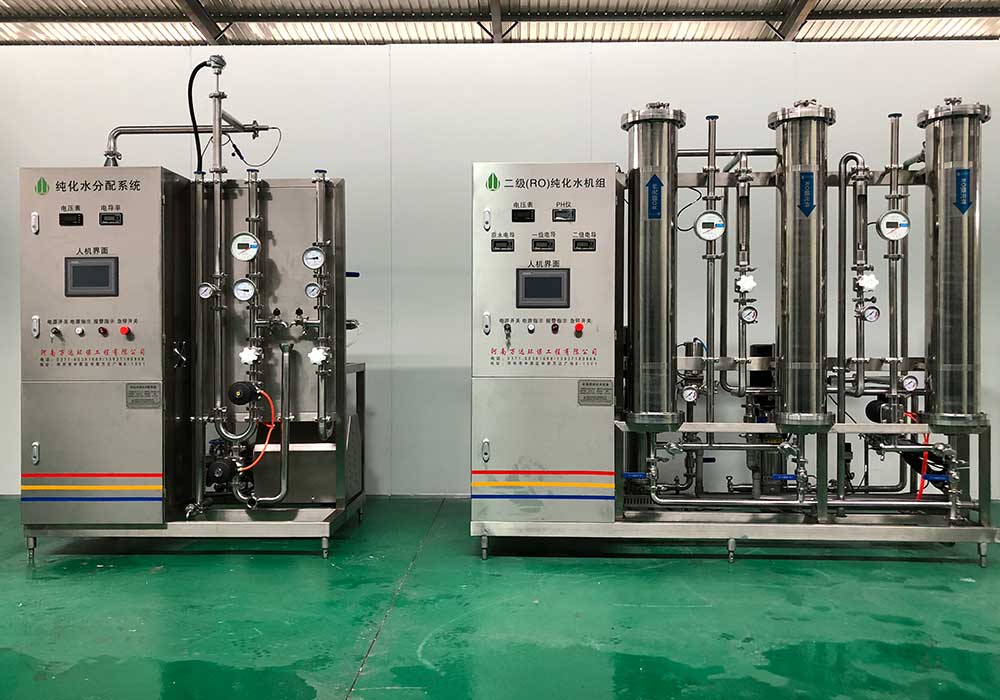
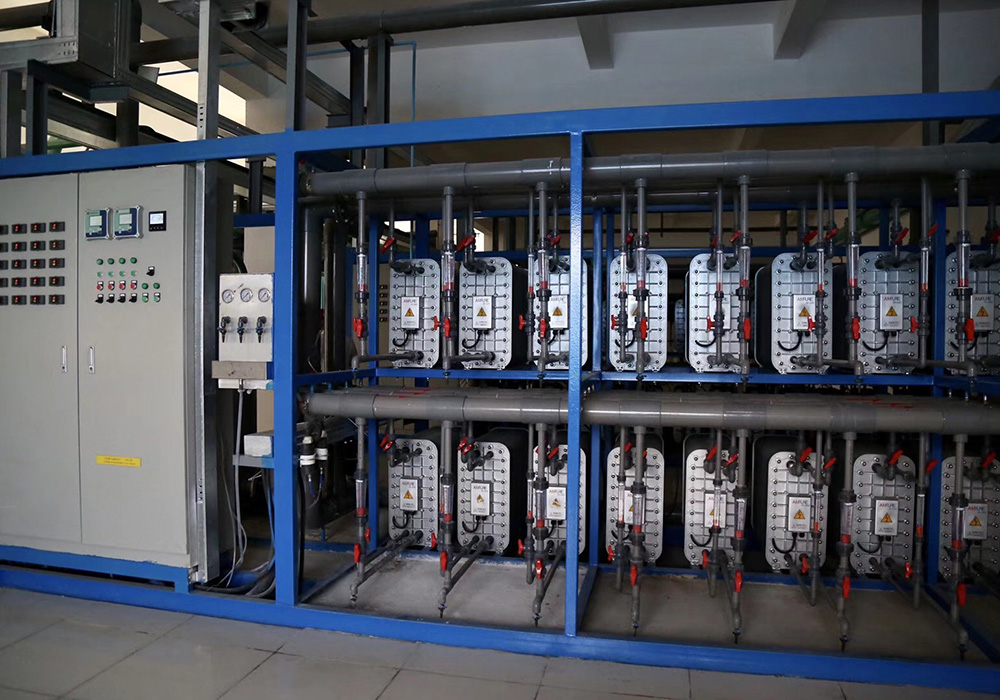
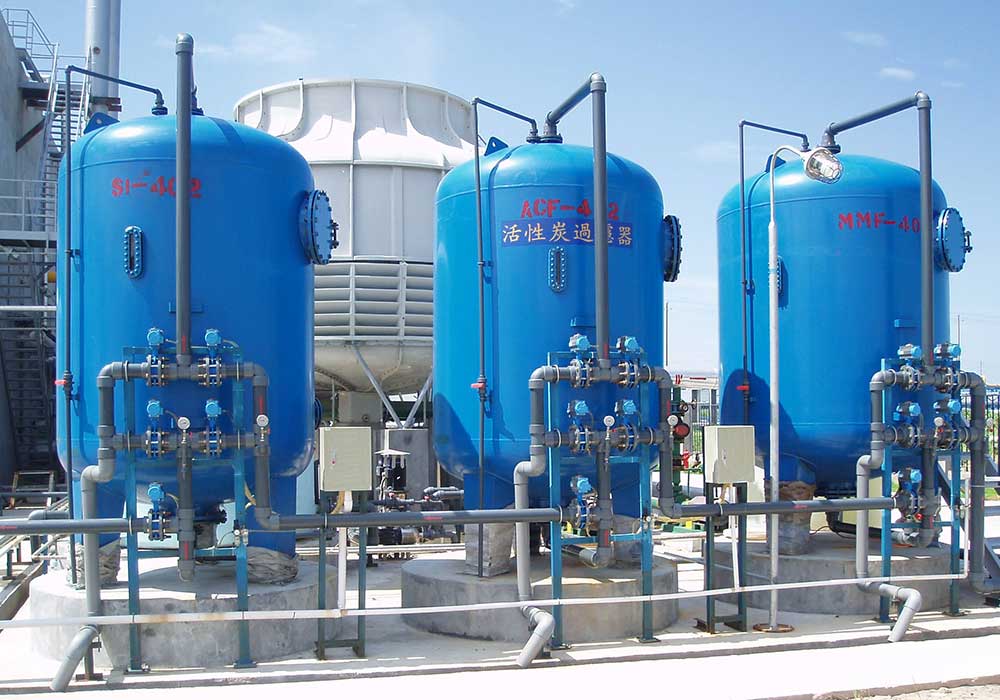
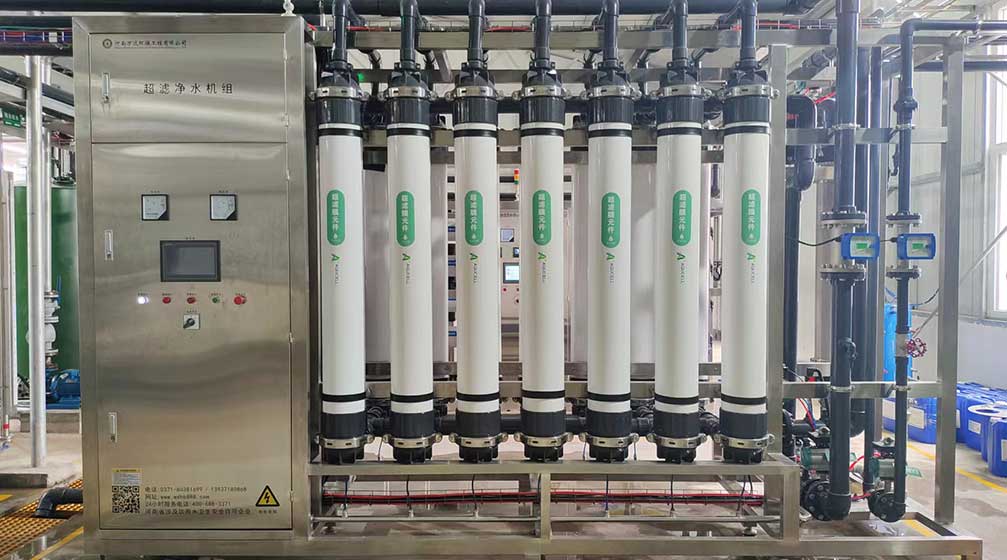
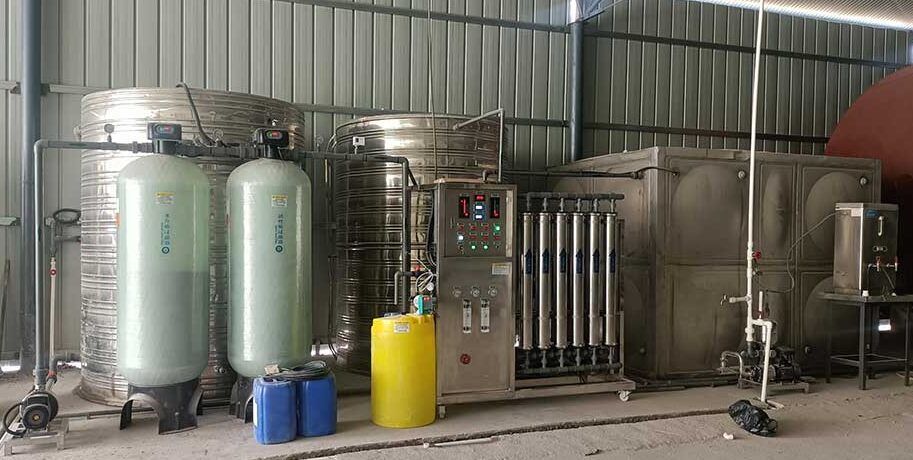
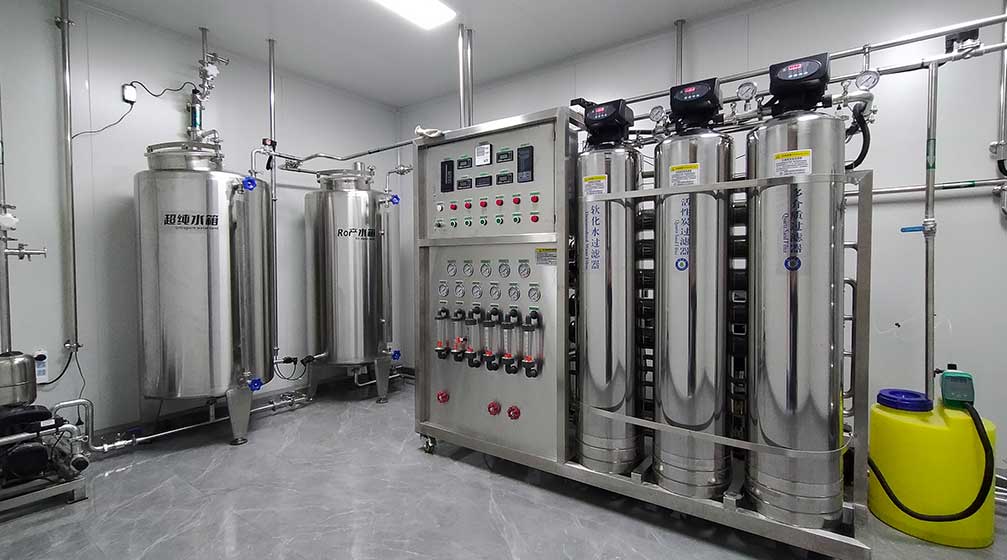
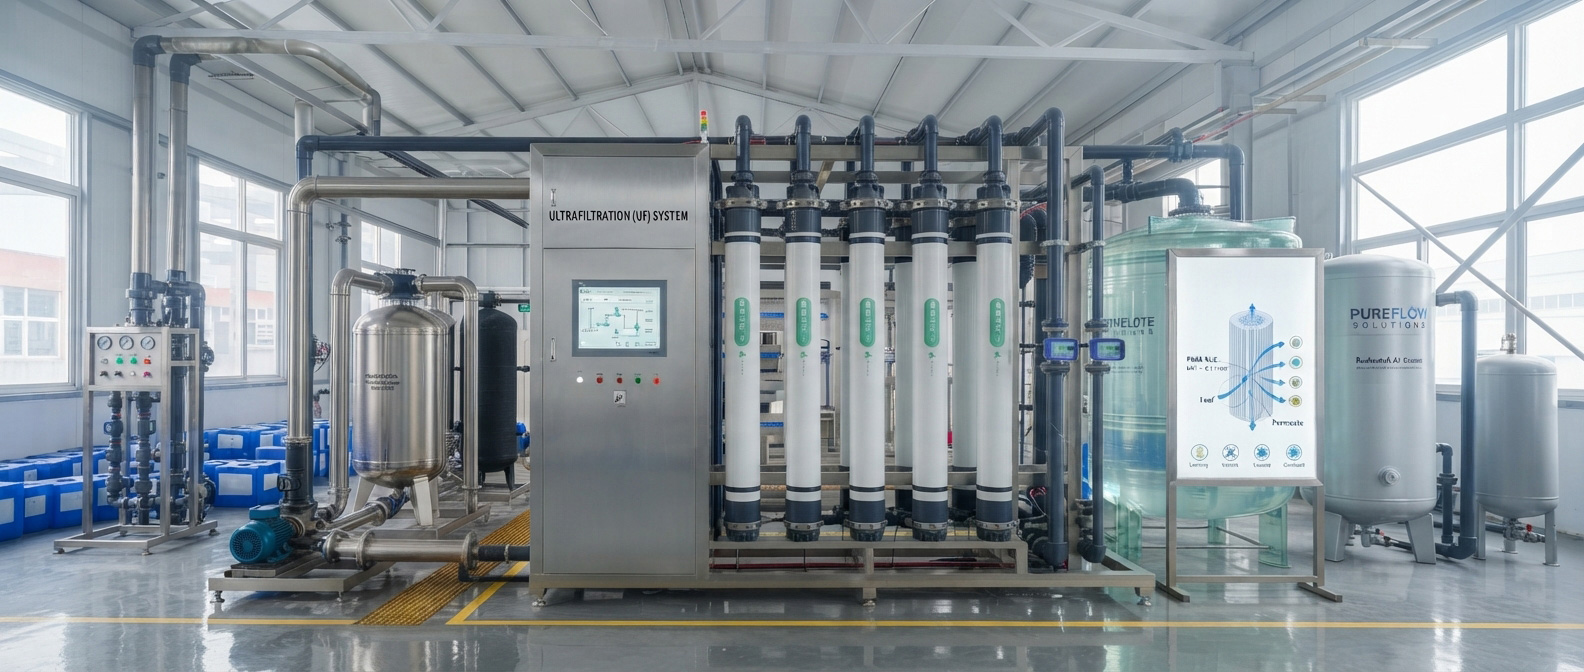
A pure water ultrafiltration system is an advanced membrane separation technology in which the solvent and various small solutes contained in the feed solution permeate through the filter membrane from the high-pressure side to the low-pressure side, thereby producing a permeate, also known as ultrafiltrate; The microporous structure of the ultrafiltration membrane can be as small as 0.01 micrometers (one hundred-thousandth of a millimeter) or smaller, effectively removing particles, colloids, bacteria, pyrogens, and organic matter from the water, while solute molecules larger than the membrane pore size are retained by the membrane and form the concentrate.
The basic principle involves filtration at room temperature under specific pressure and flow rates. Utilizing an asymmetric microporous structure and a semipermeable membrane medium, and relying on the pressure difference across the membrane as the driving force, filtration occurs via cross-flow. This allows solvents and small-molecule substances to pass through, while large-molecule substances and particles—such as proteins, water-soluble polymers, and bacteria—are retained by the filter membrane, thereby achieving the objectives of separation, classification, purification, and concentration through this novel membrane separation technology.
Product Category
Frequently Asked Questions (FAQ)
We employ a “consultative design” approach. We align deeply with your technical team during the design phase, delivering PFDs and 3D layouts to ensure the system perfectly matches your specific process constraints.
We establish a project baseline during the “Solution Finalization” phase. If adjustments are needed after the baseline is locked, we conduct an engineering impact assessment and provide a supplemental agreement, ensuring full transparency in project timelines and costs.
We adhere to a “transparency-first” principle. We provide a Bill of Materials (BOM) specifying the brand and model of all core components during the design phase, prioritizing Tier-1 global brands to ensure peak performance and global serviceability.
We adhere to rigorous quality management systems (ISO9001). For export projects, we support manufacturing compliant with international standards such as CE, UL, and ASME to meet your specific regional regulatory requirements.
For custom systems, we execute rigorous Factory Acceptance Testing (FAT). Protocols are tailor-made for your unique requirements, and we invite you to witness critical test stages via remote video. A comprehensive test report is included in the shipment.
Lead times depend on project scale and complexity. We clearly define key milestones—manufacturing, FAT, and shipping—in the contract to ensure transparent scheduling and timely project progression.
We provide 24/7 remote support via video guidance and online diagnostics. Senior engineers are available for on-site installation and commissioning services upon request.
We provide a comprehensive list of consumables upon delivery and offer full-lifecycle support. We ensure the regular supply of spare parts to prevent operational downtime.