Project Overview
Client
A leading multi-national beverage production group (Southeast Asia Branch).
Location
Bangkok, Thailand
Capacity
40,000 L/h (40 m³/h)
System Type
Heavy-Duty Single-Stage RO
Application
Natural Sweeteners & Plant Extracts
Client Background & The Challenge
A leading international manufacturer specializing in natural food ingredients—including natural pigments, D-Allulose (D-阿洛酮糖), natural sweeteners, plant extracts, coloring foods, and natural antioxidants—established a large-scale production facility in Bangkok, Thailand.
- High-Volume Process Demand: The continuous extraction, refinement, and concentration of sensitive bio-compounds required a stable, heavy-duty 40 m³/h water supply to maintain uninterrupted production schedules.
- Strict Purity & Low Conductivity: Processing functional sweeteners and plant extracts demanded high-purity water free from mineral scaling and trace organic impurities that could affect product quality.
- System Reliability & Durability: The facility required a robust single-stage RO system capable of sustained, 24/7 heavy industrial operation while minimizing membrane fouling and maintenance downtime.
Our Solution
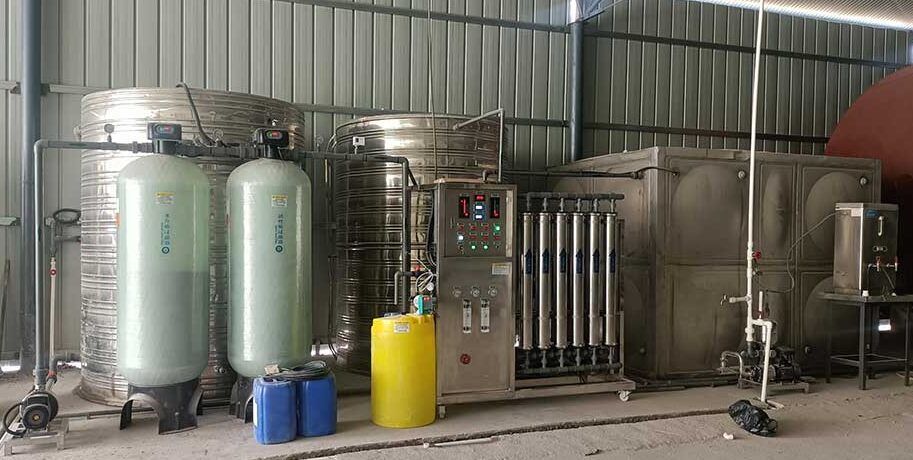
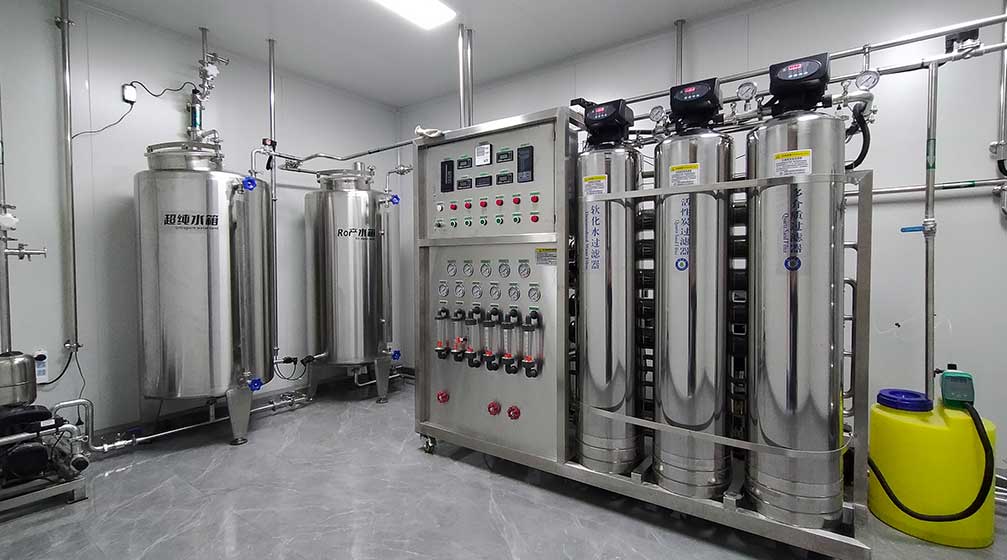
We engineered a high-capacity, heavy-duty single-stage reverse osmosis system optimized for the stringent requirements of natural food additives:
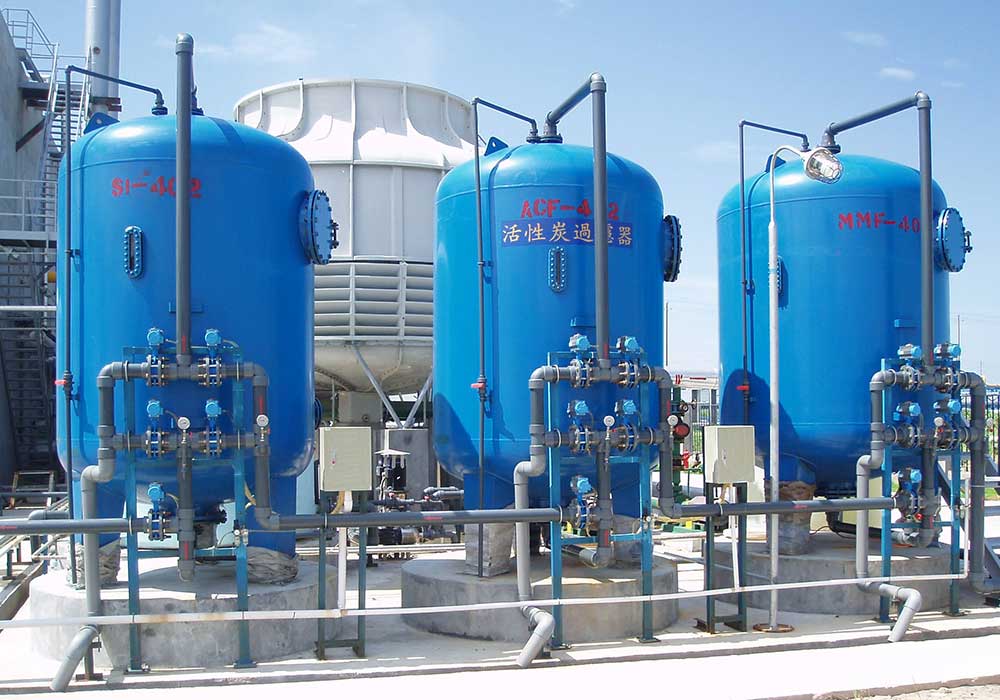
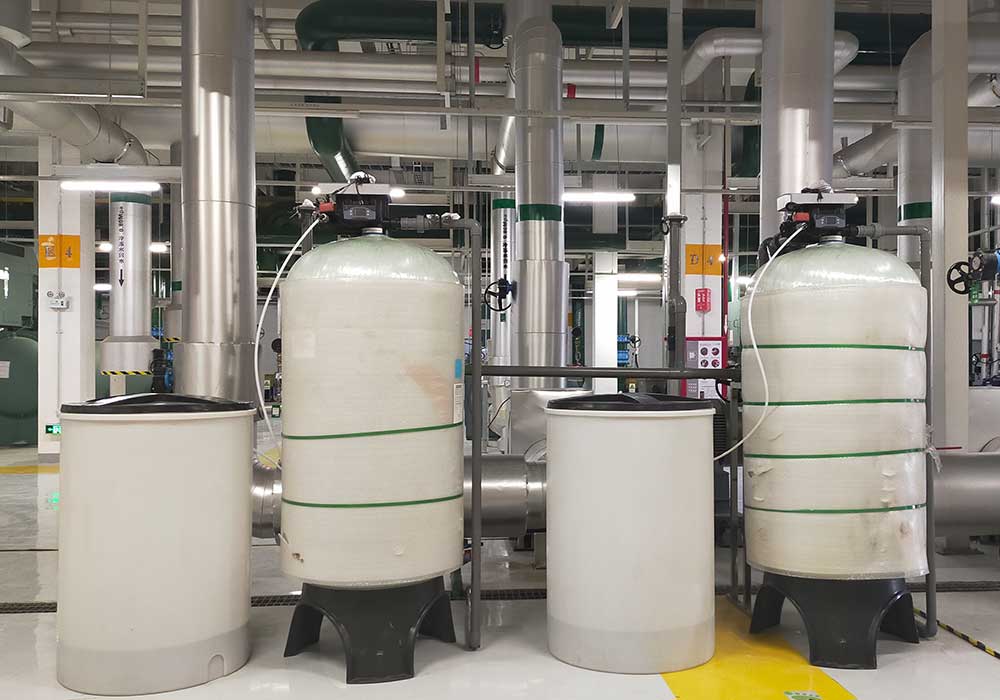
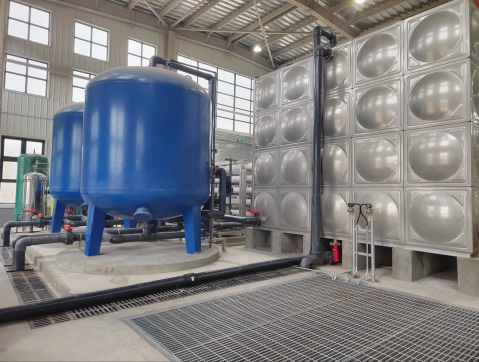
Robust Pre-treatment Phase
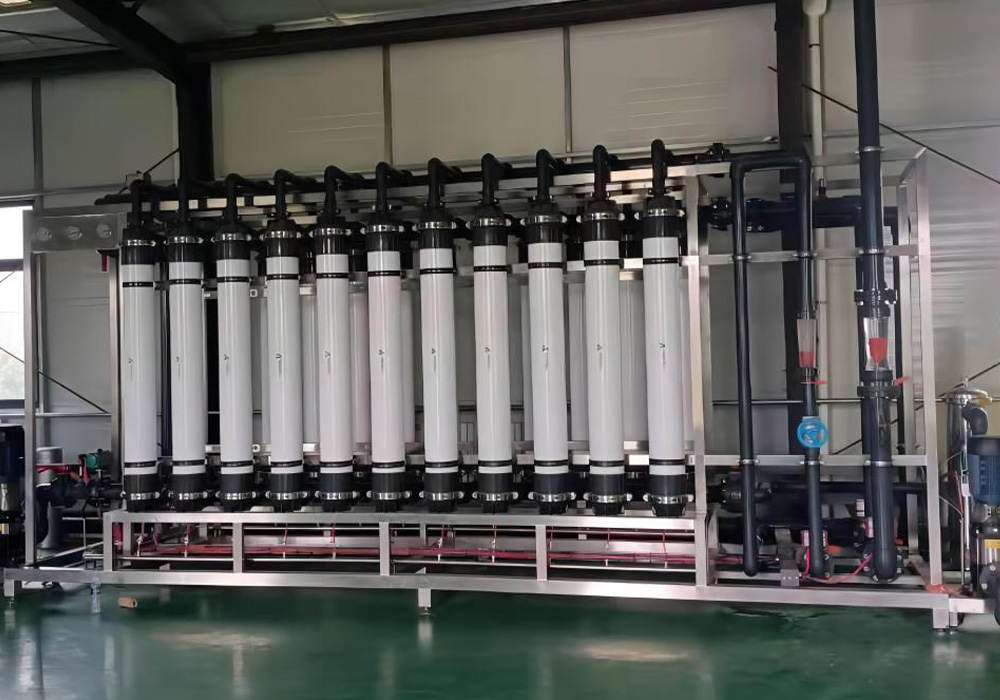
We engineered a high-capacity, heavy-duty single-stage reverse osmosis system optimized for the stringent requirements of natural food additives:
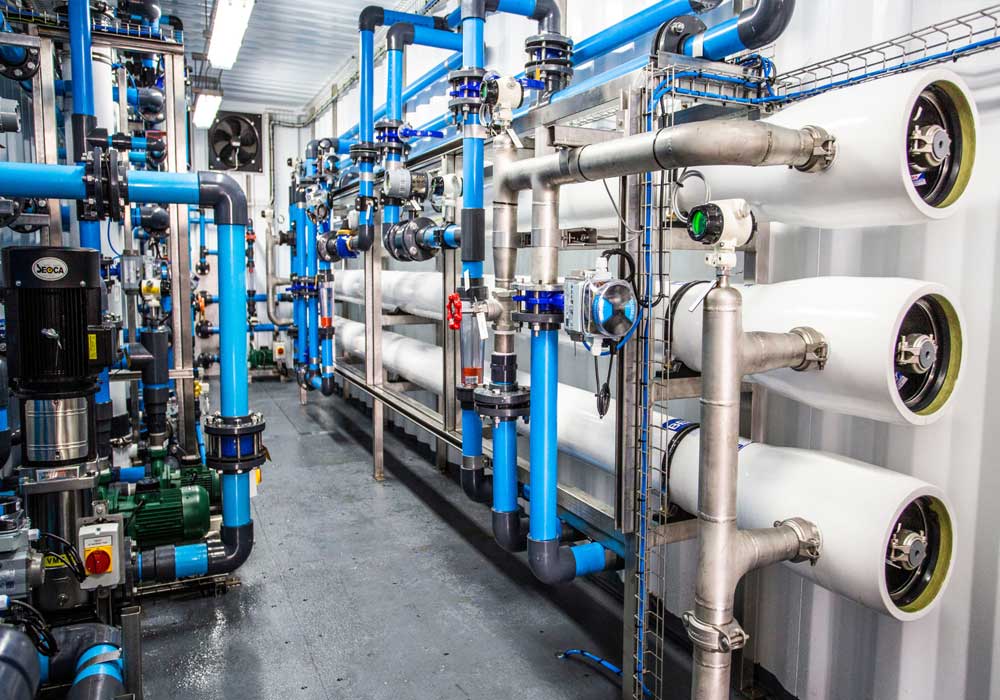
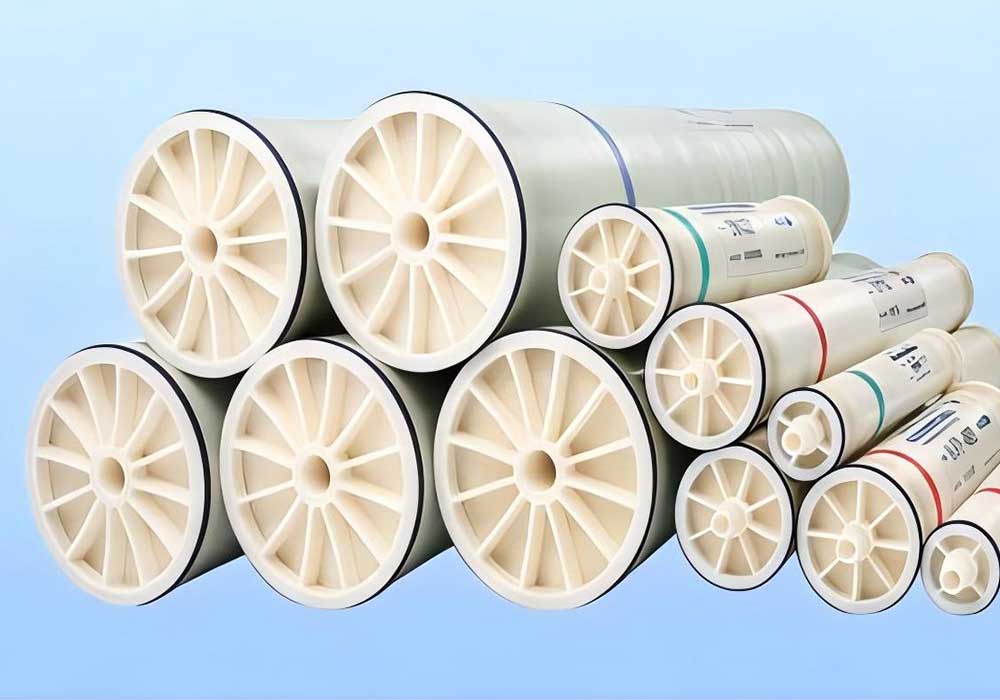
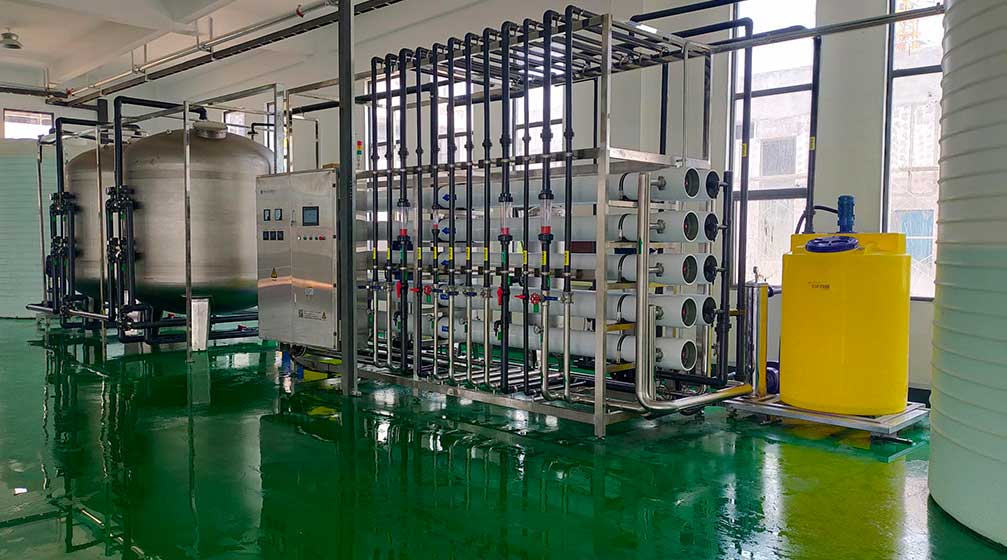
High-Capacity Single-Stage RO Core
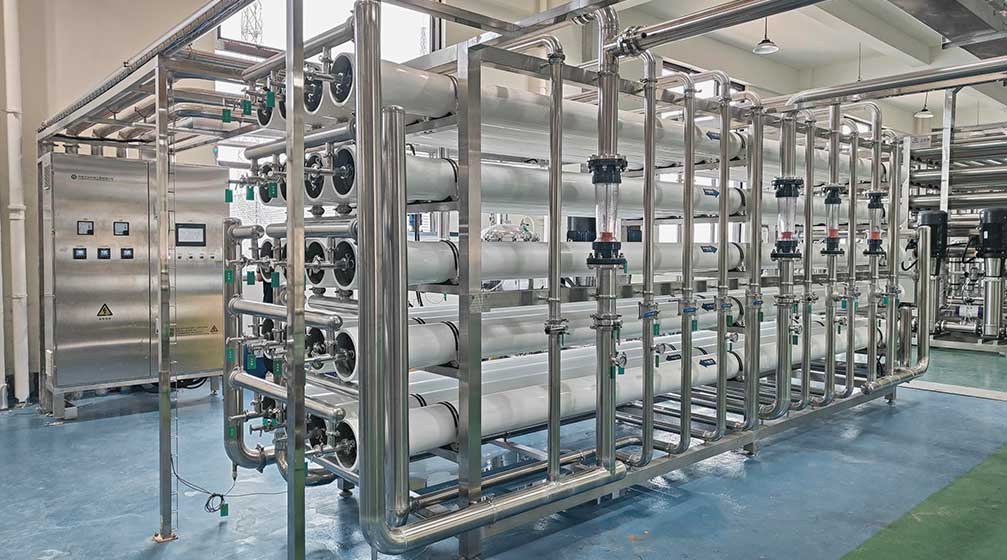
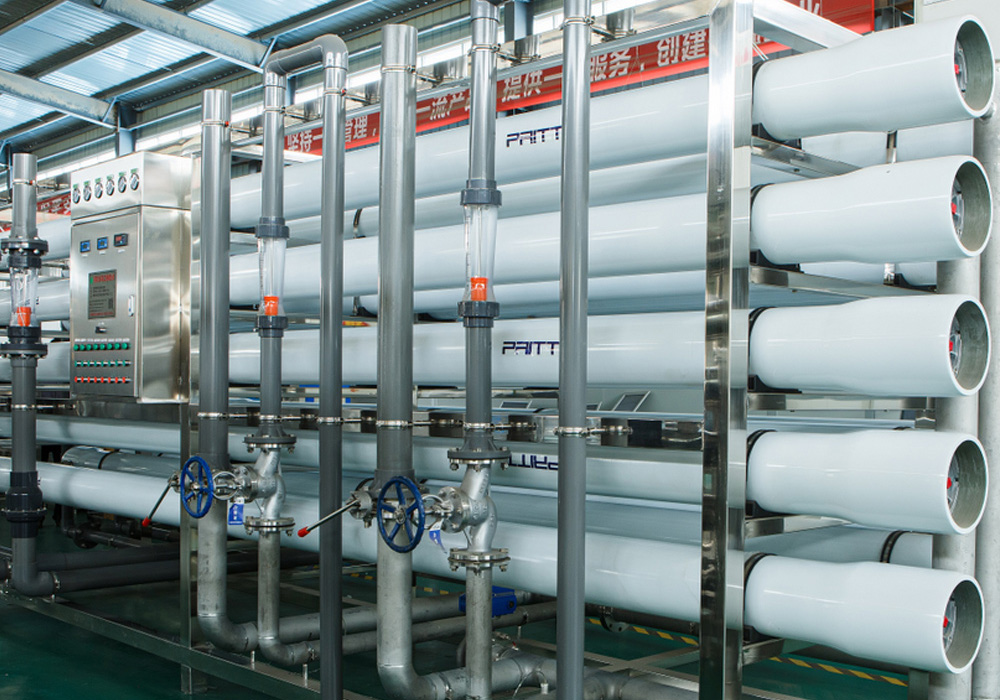
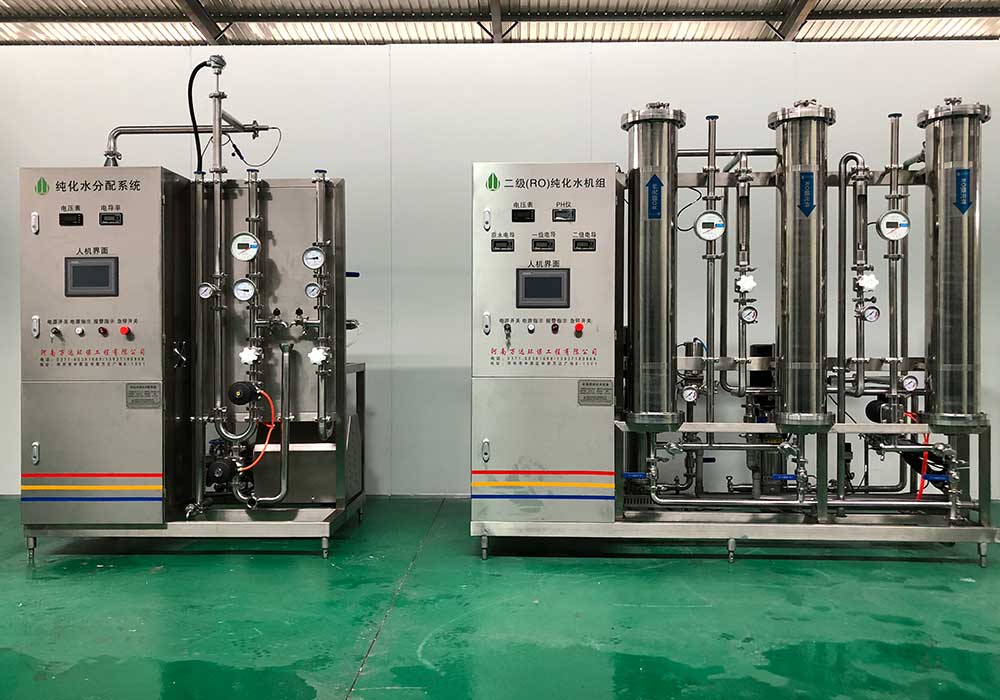
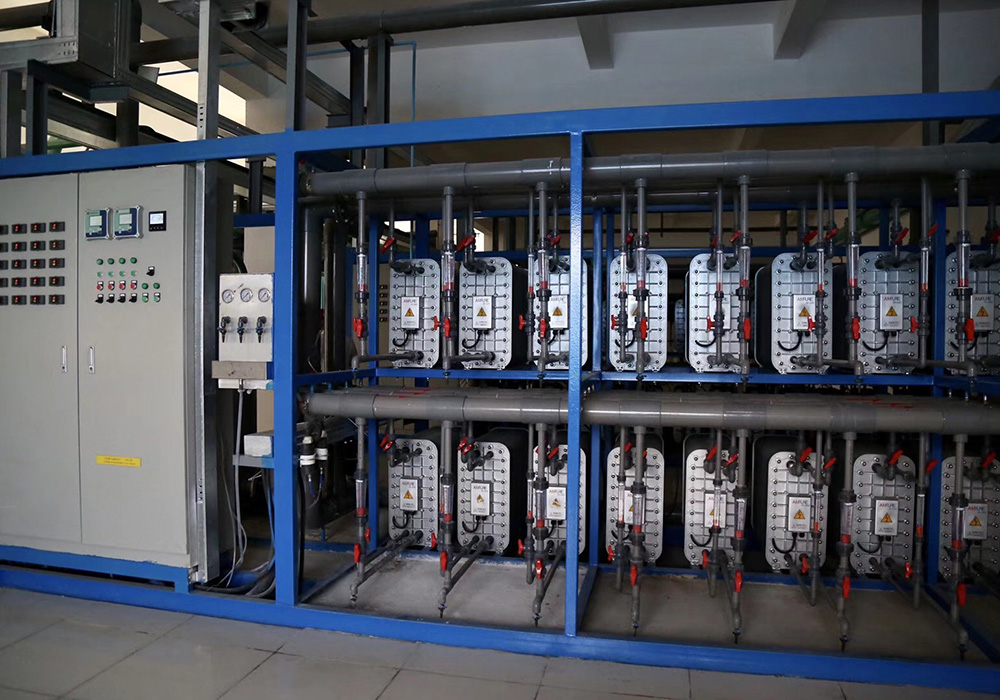
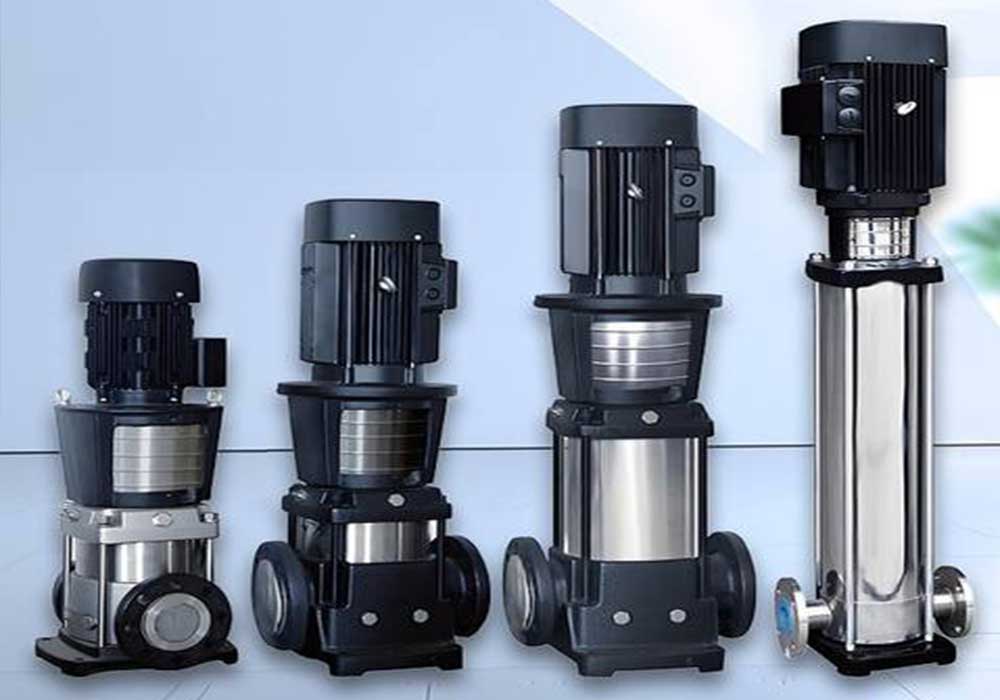
Deployed a high-efficiency single-stage RO host paired with heavy-duty stainless steel pressure pumps, delivering a reliable 40 m³/h permeate flow with high desalination performance.
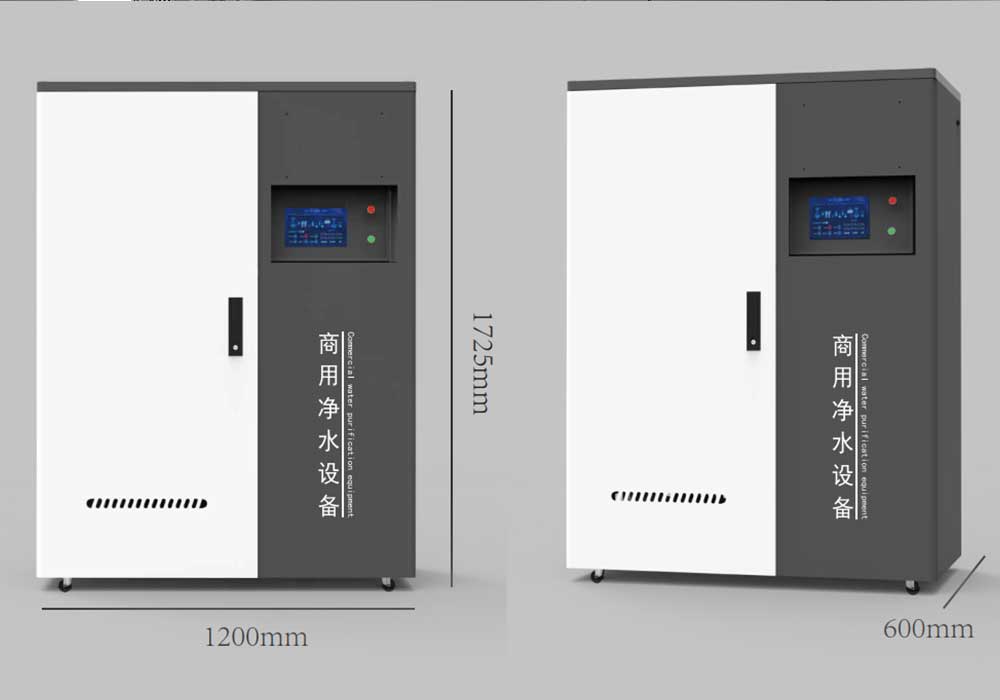
Sanitary Integration & Control
Designed with corrosion-resistant components, clean-in-place (CIP) compatibility, and an automated PLC-HMI interface to ensure precise monitoring and easy sanitation between batches.
Project Results & Benefits
Following successful installation and commissioning, the 40 m³/h single-stage RO system delivered exceptional operational stability, continuously supplying high-purity water that significantly enhanced the extraction yield and clarity of natural pigments, D-Allulose, and plant extracts. The robust pre-treatment and automated dosing configuration successfully mitigated membrane scaling, ensuring continuous 24/7 manufacturing safety while lowering long-term operational and maintenance overhead.
Technical Specifications
| APPLICABLE WATER SOURCE | Municipal tap water, industrial groundwater for ingredient extraction and processing. |
| INFULENT QUALITY | TDS<500ppm,SDI<3, Free Chlorine<0.1ppm |
| PRODUCTION WATER QUALITY | Conductivity<5μS/cm, iptimized for natural extract and sweetener processing |
| WORKING VOLTAGE | AC 380V/50HZ 3P or AC 415V/50HZ 3P (customizable forindustrial standards) |
| WORKING PRESSURE | Pre processing: 0.2-0.4Mpa, RO host: 0.7-1.8Mpa |
| DESALINATION RATE | 95% – 99% (NOTE: Rate varies with temperature, pressure, andfouling) |
| RECOVERY RATE | 60% – 75% (Subject to temperature, pressure, and membraneconditions) Steel Piping |
| OPTINAL ADD-ONS | CIP Cleaning System /UV Sterilizers / Stainless |