Smart Commercial Water Vending Stations
Empower your business with IoT-enabled, coin/card/cashless-operated water vending solutions designed for high-traffic indoor and outdoor locations.
Commercial Water Vending Stations
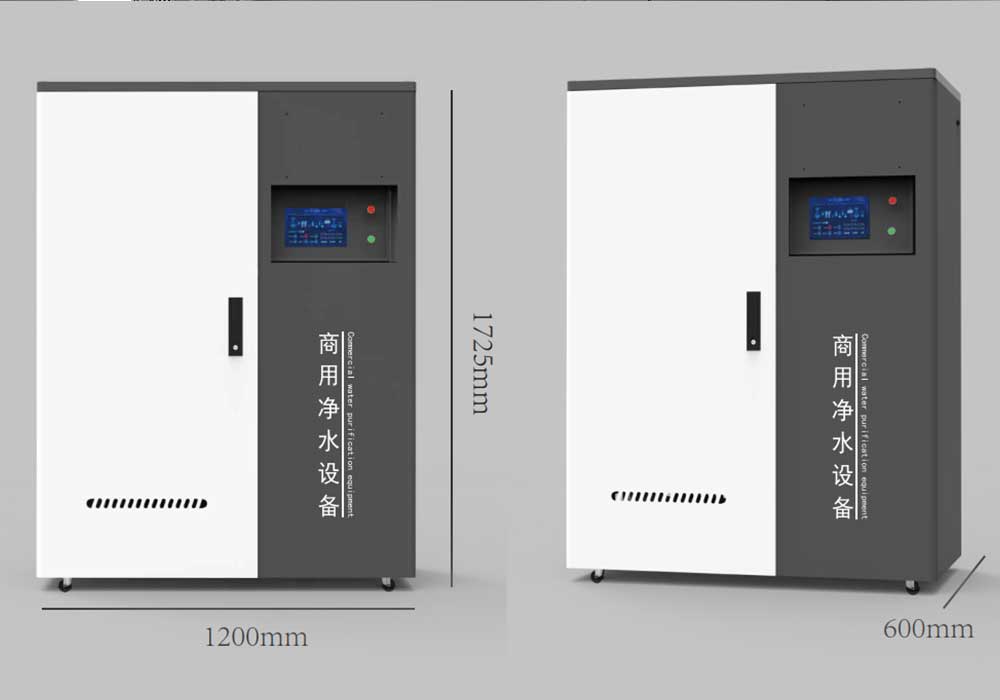
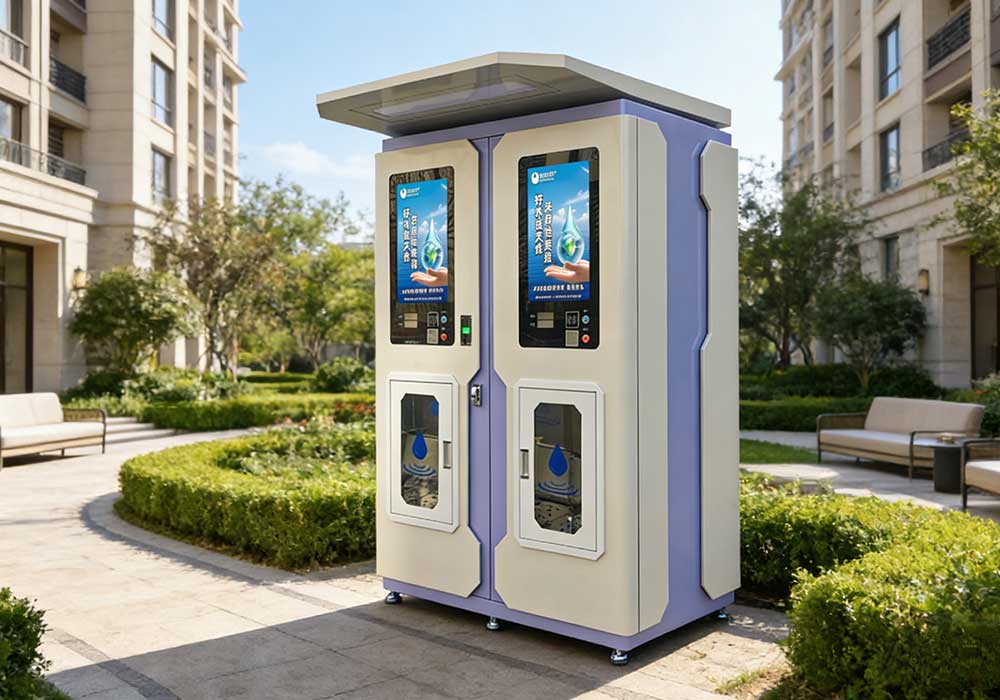
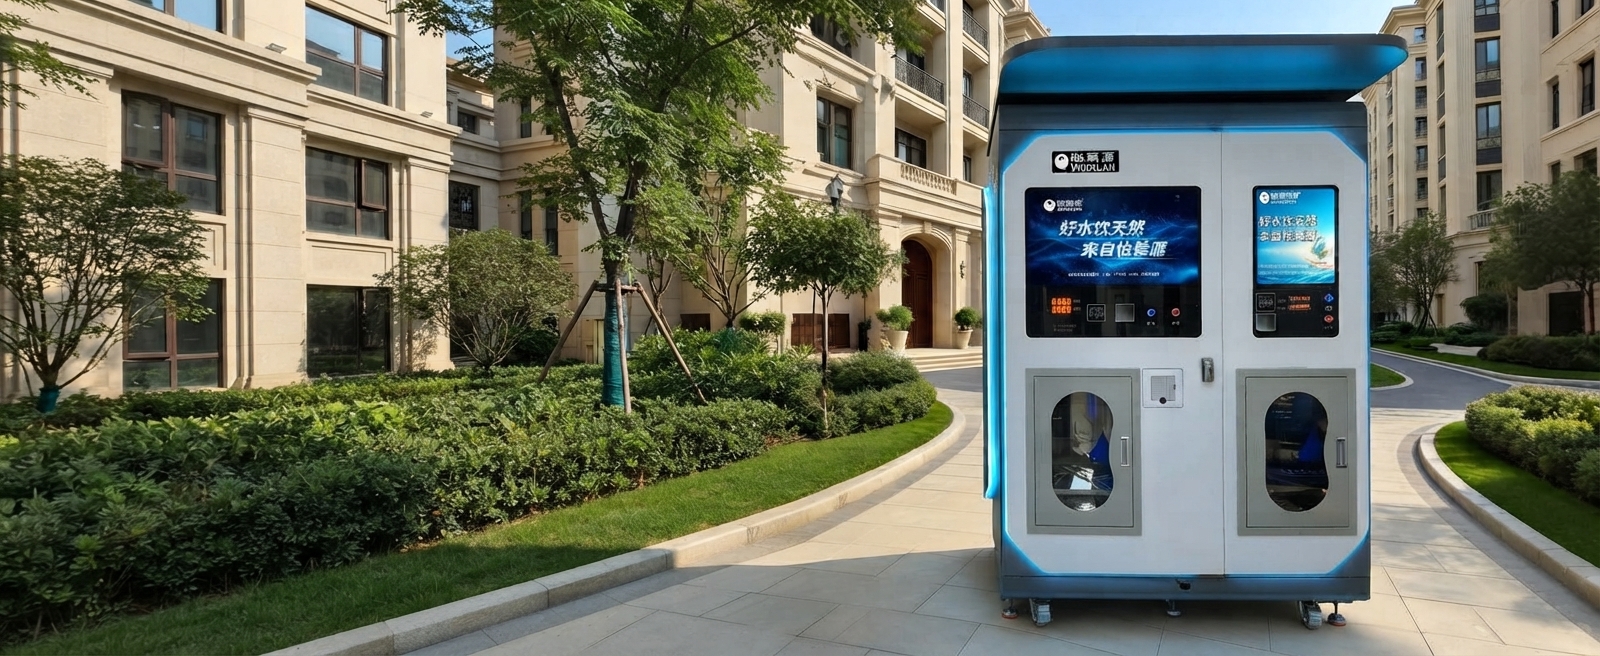
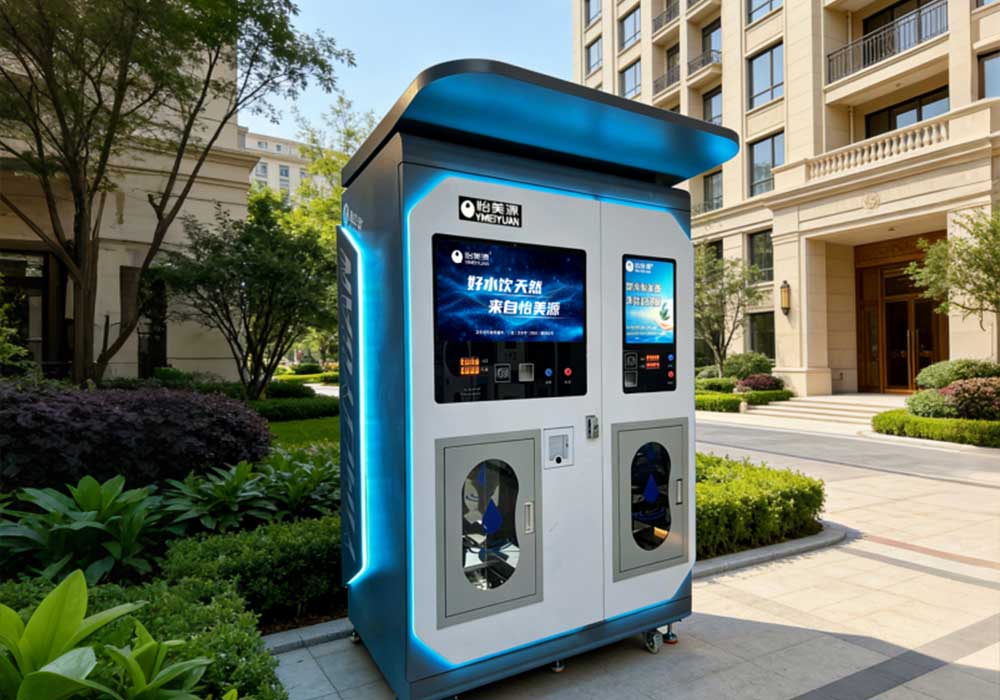
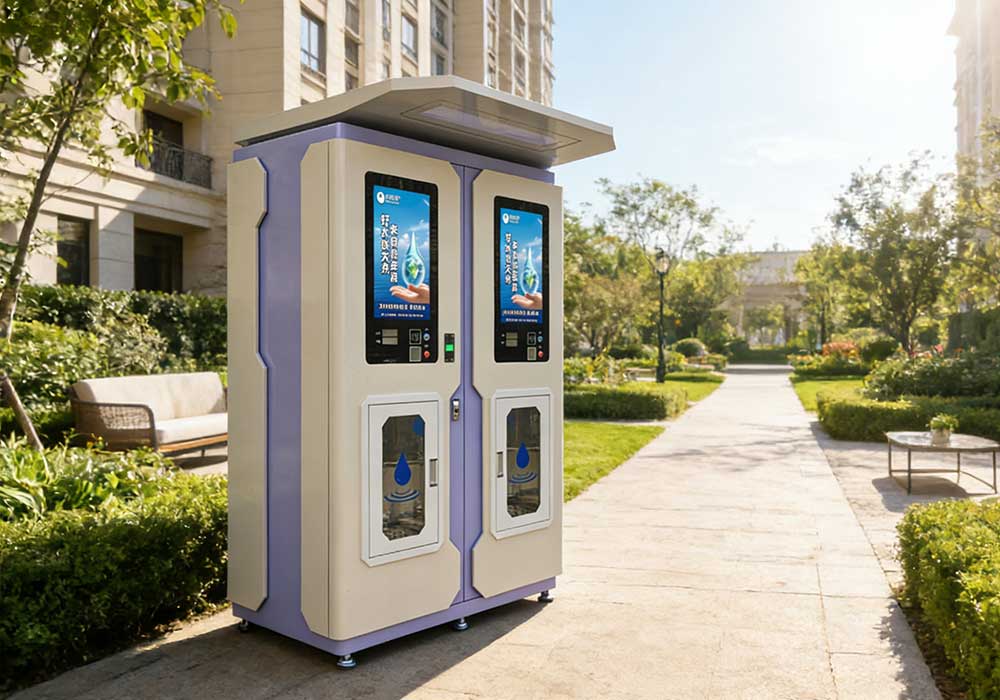
Engineered for high-traffic public locations, residential communities, and outdoor spaces, our smart water vending stations provide safe, great-tasting, purified drinking water on demand. Designed for maximum reliability and ease of operation, they offer a profitable self-service business model for operators worldwide.
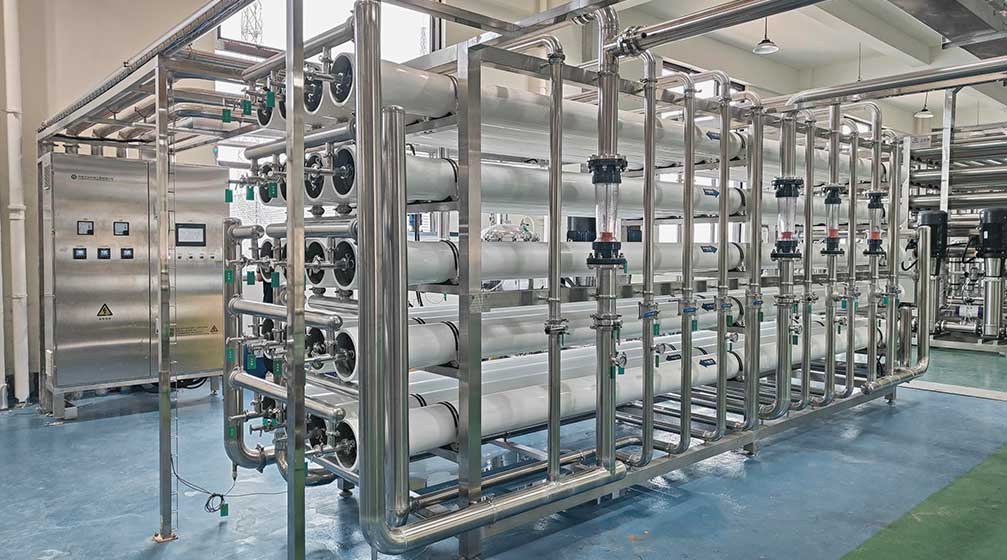
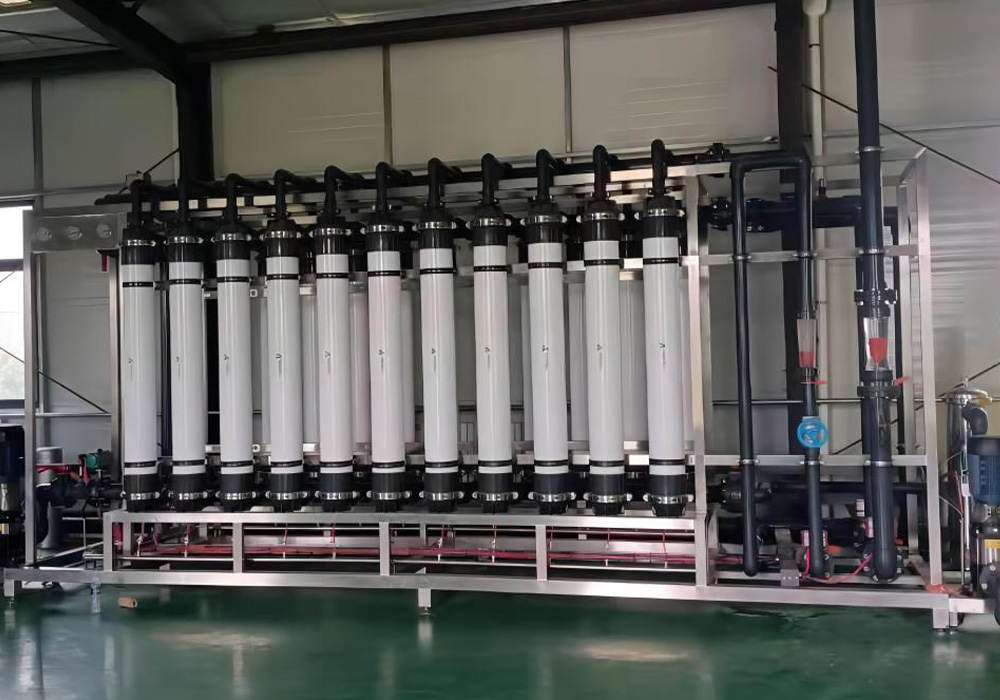
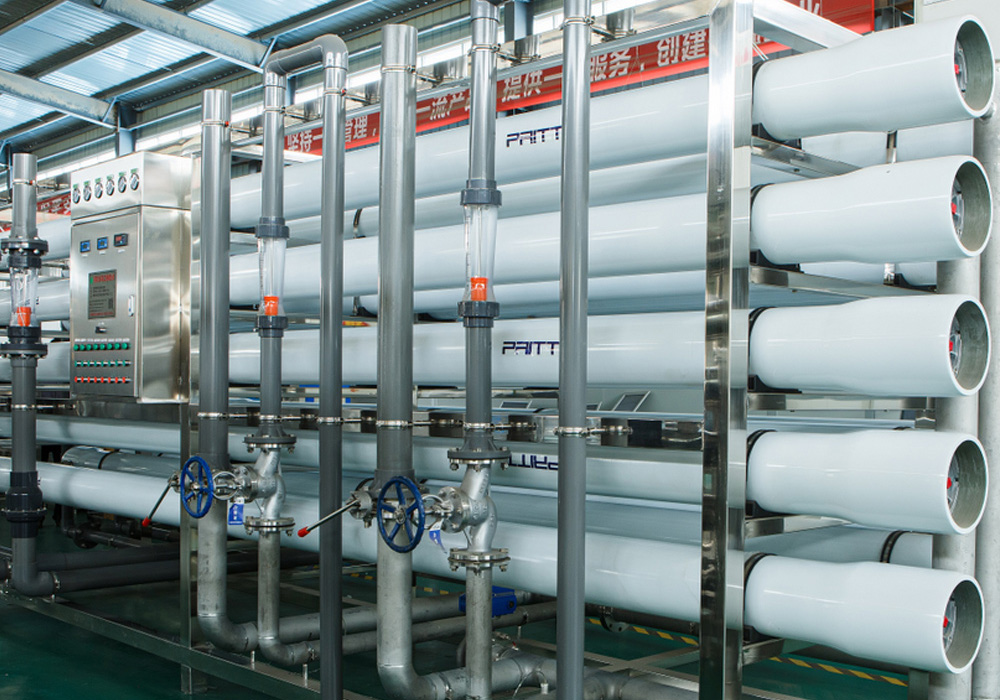
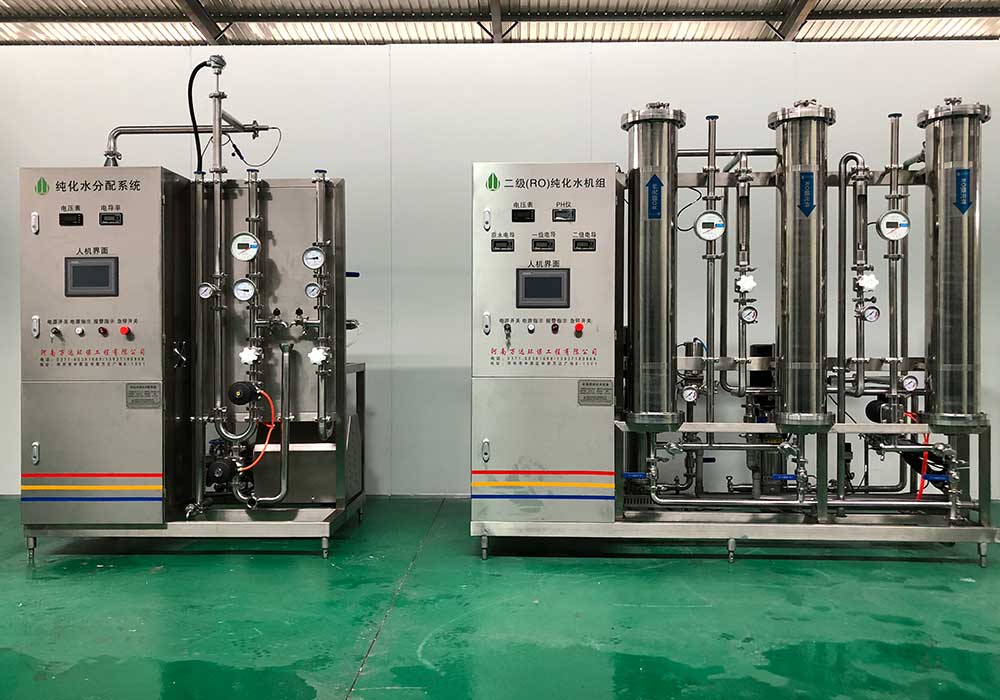
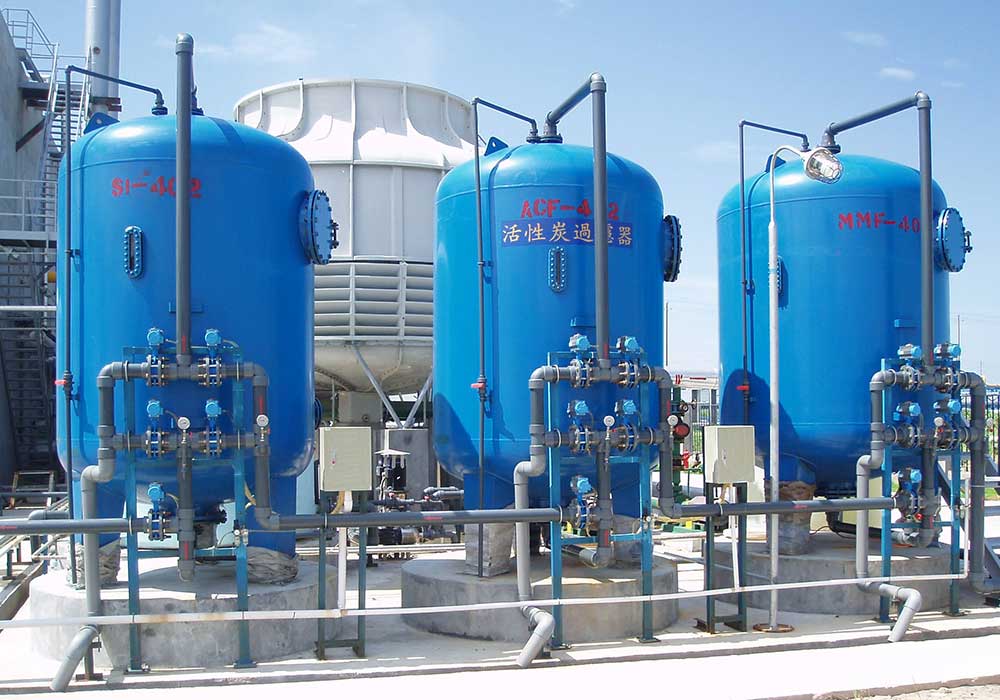
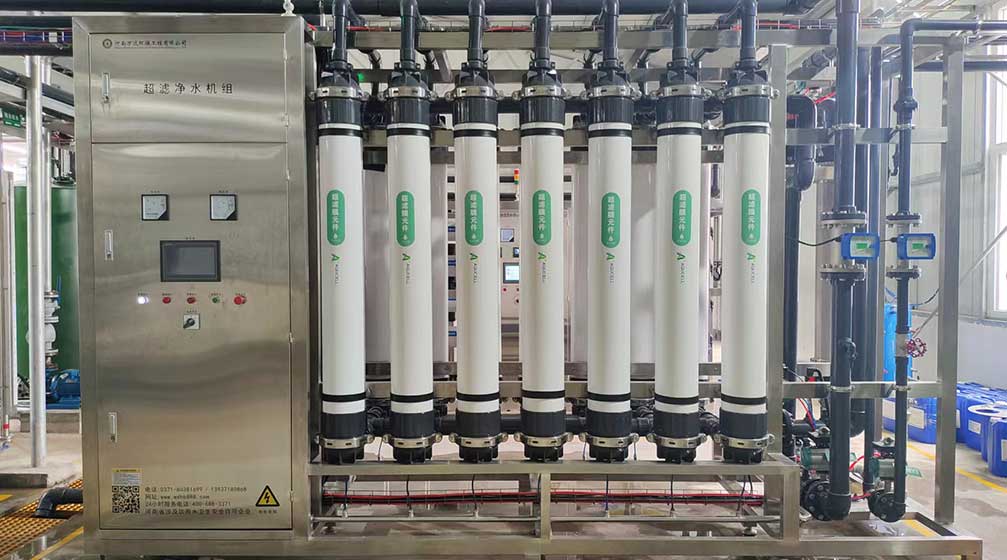
Advanced Multi-Stage Purification: Integrated Reverse Osmosis (RO) or Ultrafiltration (UF) systems effectively eliminate impurities, heavy metals, and bacteria, ensuring strict adherence to drinking water standards.
Flexible Payment Integration: Supports multi-coin acceptors, bill validators, and modern cashless payment modules (RFID smart cards, QR code mobile payments) for user convenience.
Rugged & Weather-Resistant Build: Constructed with heavy-duty, anti-rust steel cabinets designed to withstand harsh outdoor weather conditions and heavy public use.
Smart IoT Remote Monitoring: Optional cloud-based management system allows operators to monitor water quality, filter life span, and daily sales data in real time.
High-Capacity Dispensing: Features reinforced delivery windows and robust pumps designed to accommodate large containers, such as 5-gallon jugs and individual bottles.
Product Classification
Frequently Asked Questions (FAQ)
We employ a “consultative design” approach. We align deeply with your technical team during the design phase, delivering PFDs and 3D layouts to ensure the system perfectly matches your specific process constraints.
We establish a project baseline during the “Solution Finalization” phase. If adjustments are needed after the baseline is locked, we conduct an engineering impact assessment and provide a supplemental agreement, ensuring full transparency in project timelines and costs.
We adhere to a “transparency-first” principle. We provide a Bill of Materials (BOM) specifying the brand and model of all core components during the design phase, prioritizing Tier-1 global brands to ensure peak performance and global serviceability.
We adhere to rigorous quality management systems (ISO9001). For export projects, we support manufacturing compliant with international standards such as CE, UL, and ASME to meet your specific regional regulatory requirements.
For custom systems, we execute rigorous Factory Acceptance Testing (FAT). Protocols are tailor-made for your unique requirements, and we invite you to witness critical test stages via remote video. A comprehensive test report is included in the shipment.
Lead times depend on project scale and complexity. We clearly define key milestones—manufacturing, FAT, and shipping—in the contract to ensure transparent scheduling and timely project progression.
We provide 24/7 remote support via video guidance and online diagnostics. Senior engineers are available for on-site installation and commissioning services upon request.
We provide a comprehensive list of consumables upon delivery and offer full-lifecycle support. We ensure the regular supply of spare parts to prevent operational downtime.