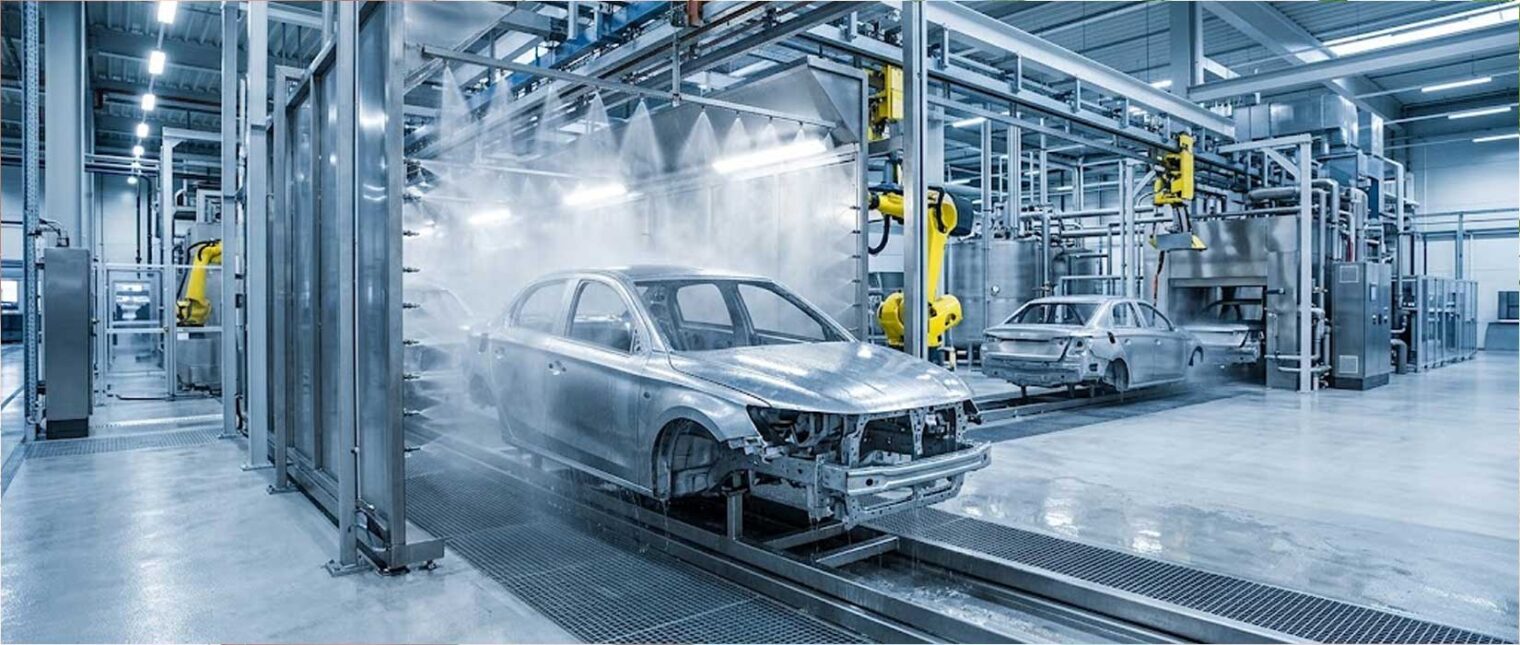
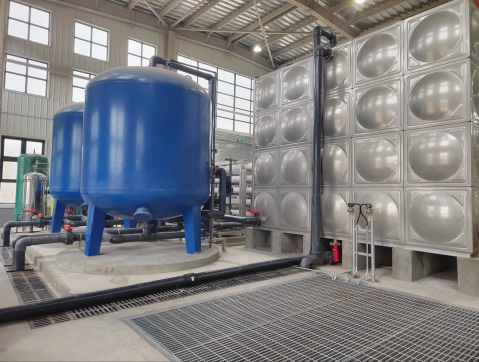
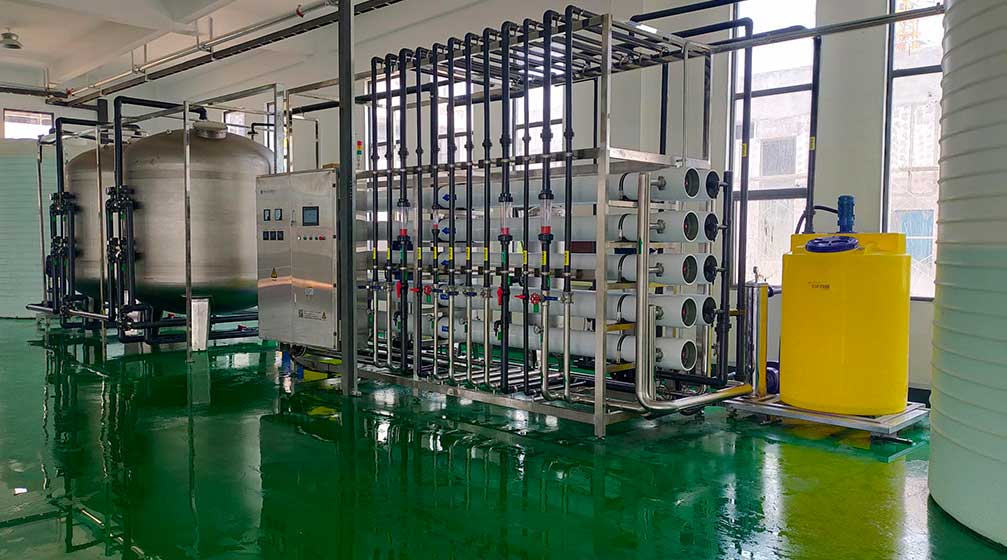
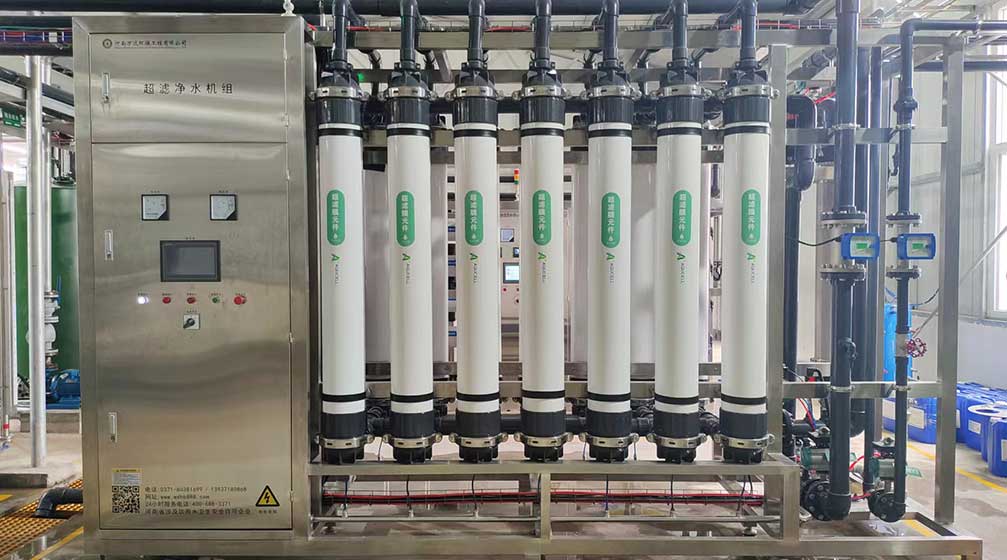
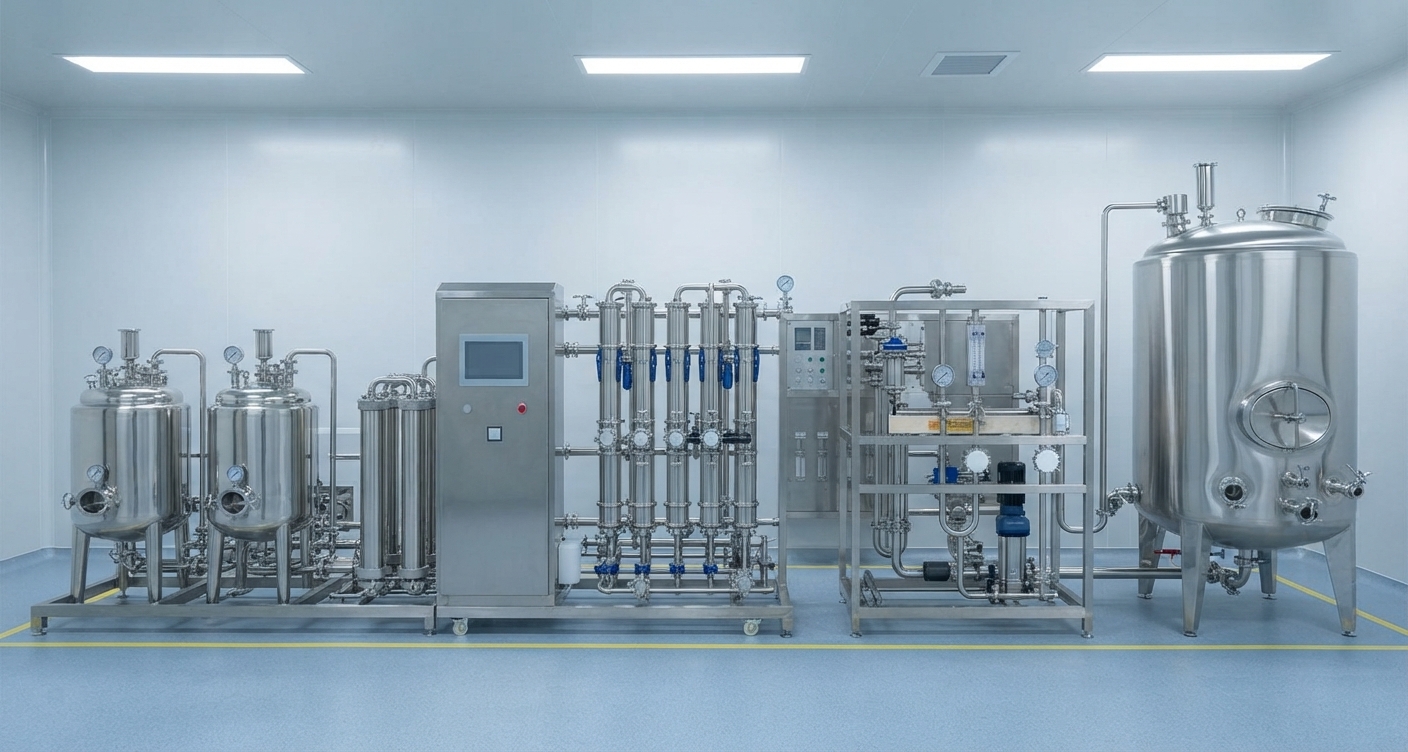
GMP Pharmaceutical Purified Water Systems
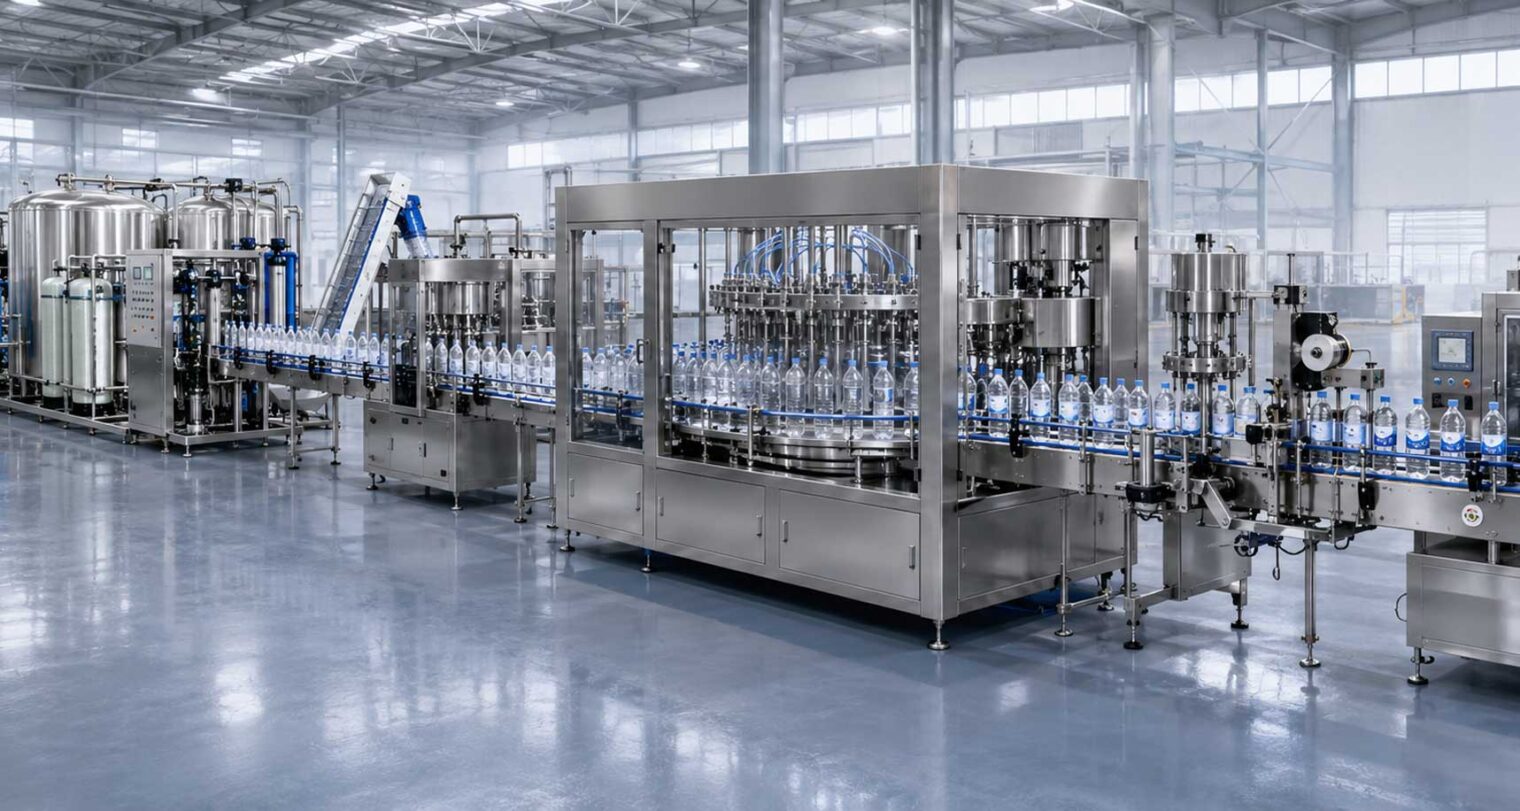
Engineered to meet rigorous pharmacopeia standards, featuring full sanitary stainless steel construction and reliable high-purity water generation for biotech and pharmaceutical applications.
Reverse Osmosis Water Filtration Machine manufacturer
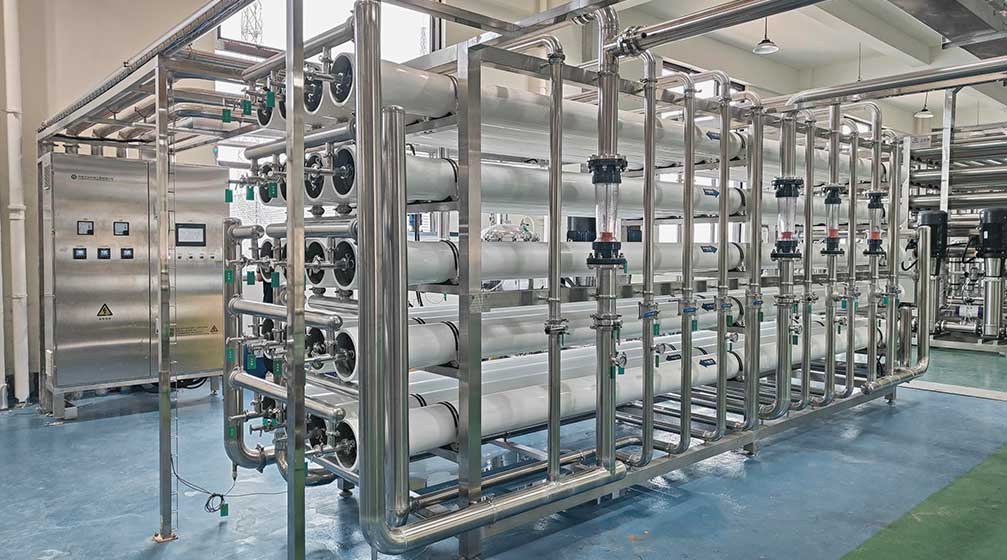
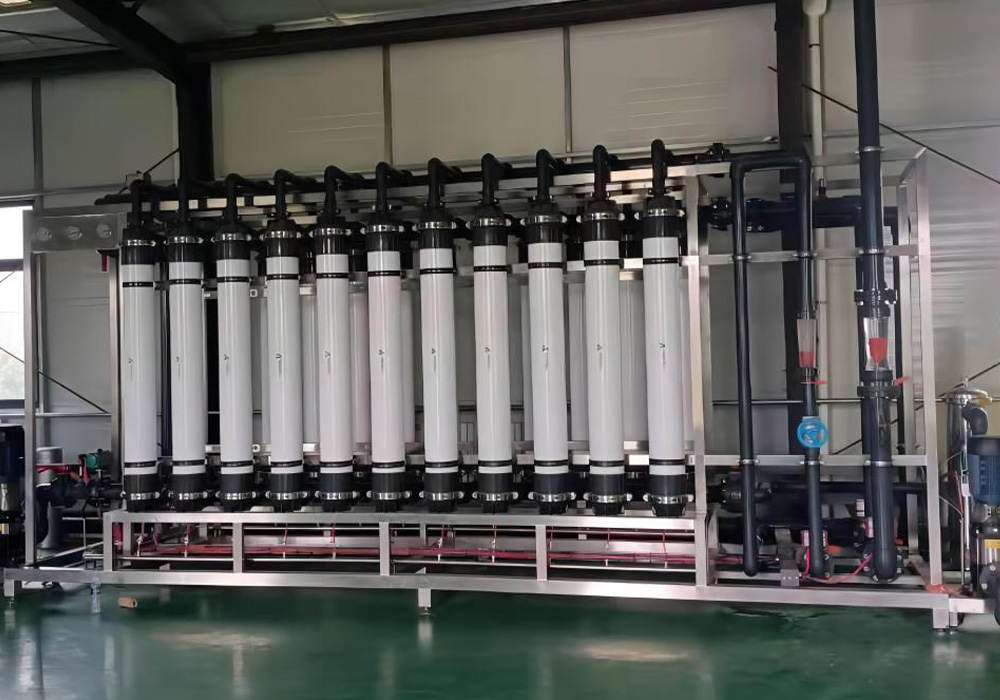
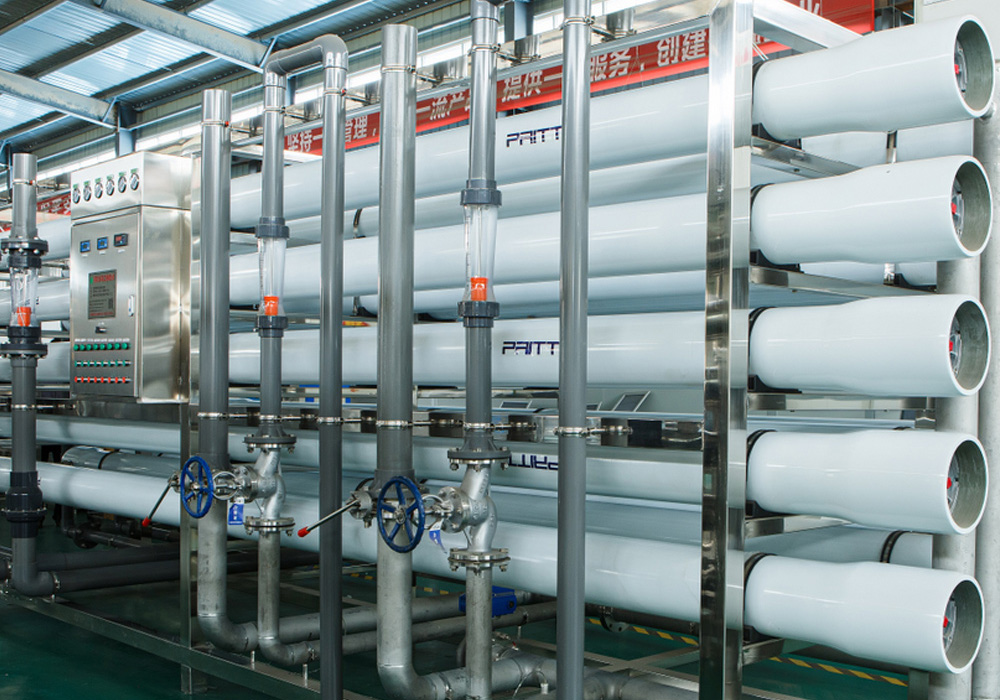
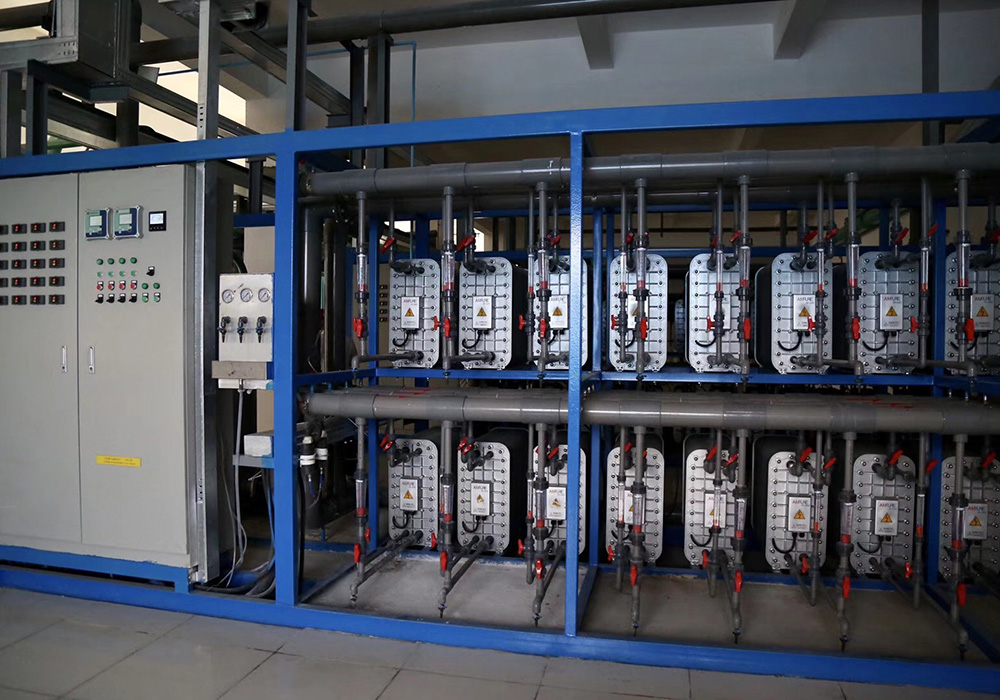
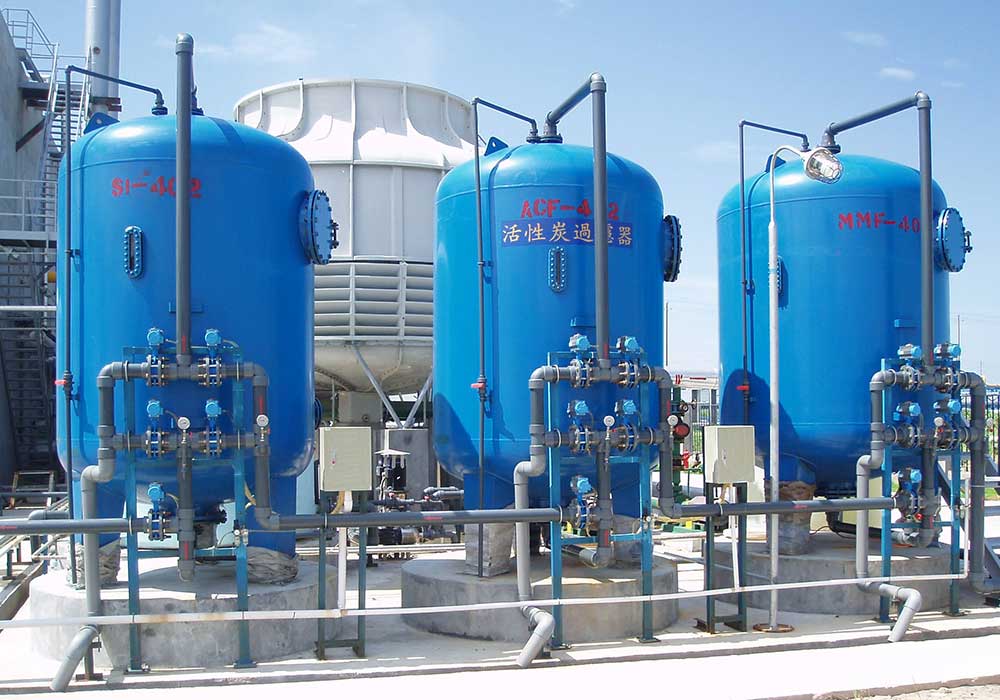
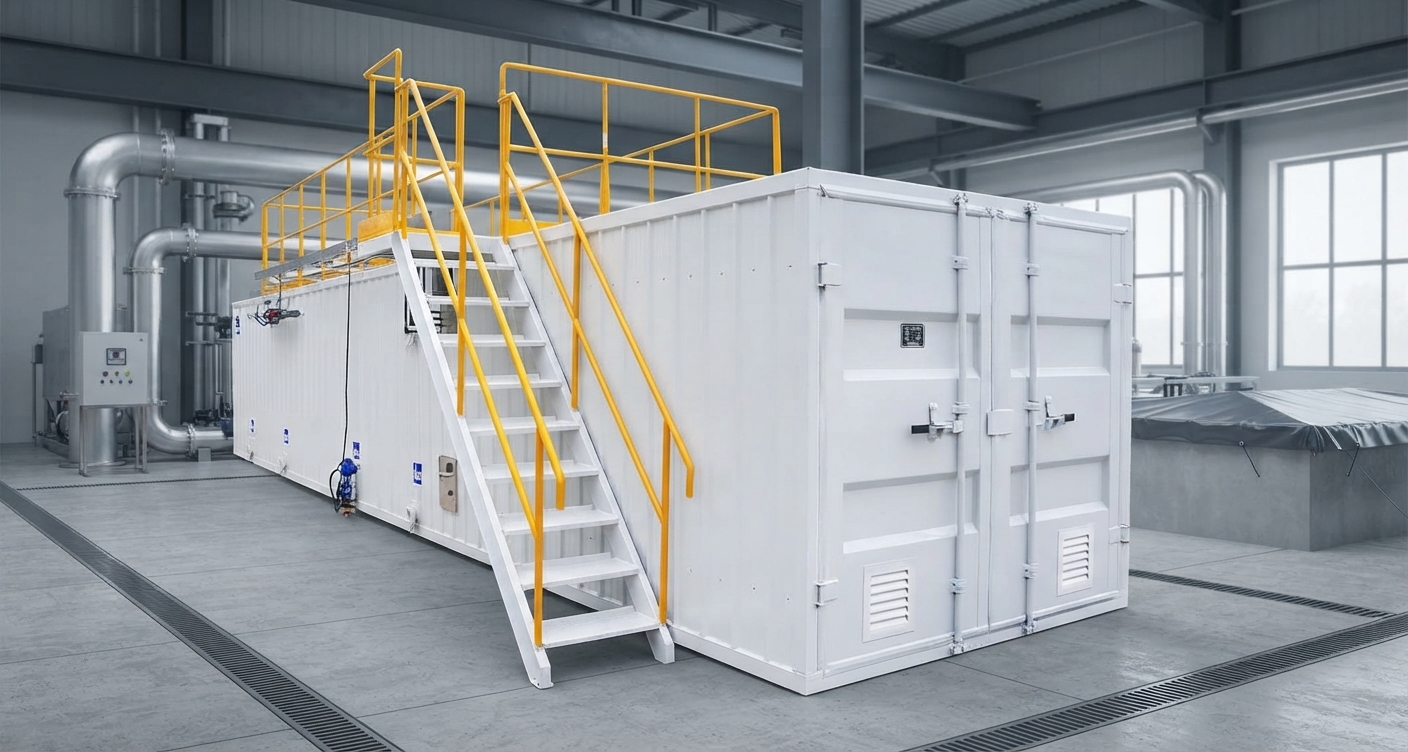
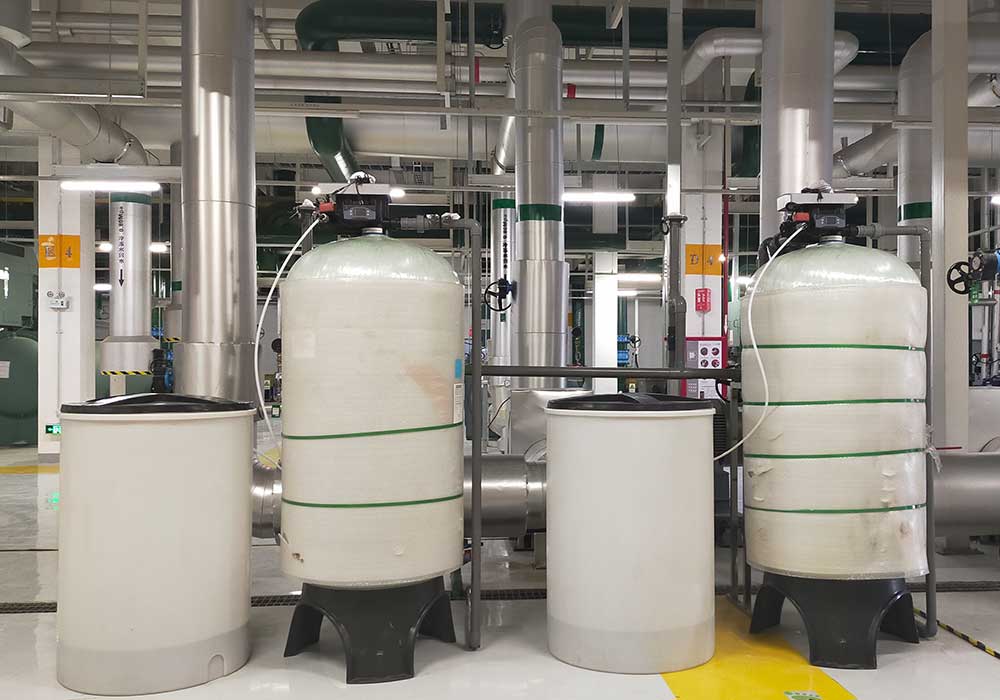
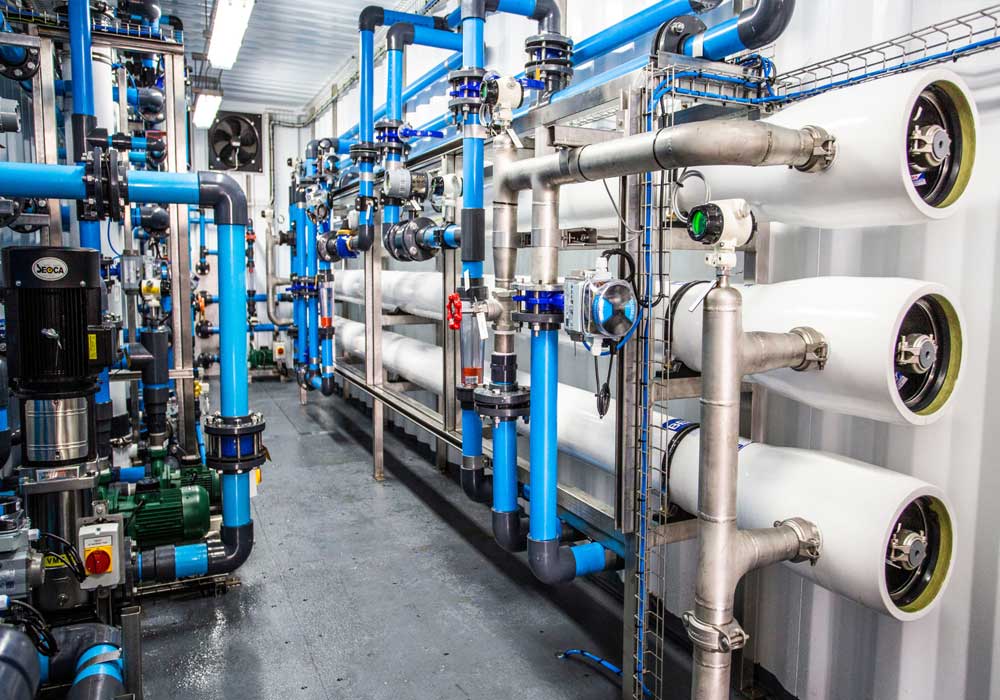
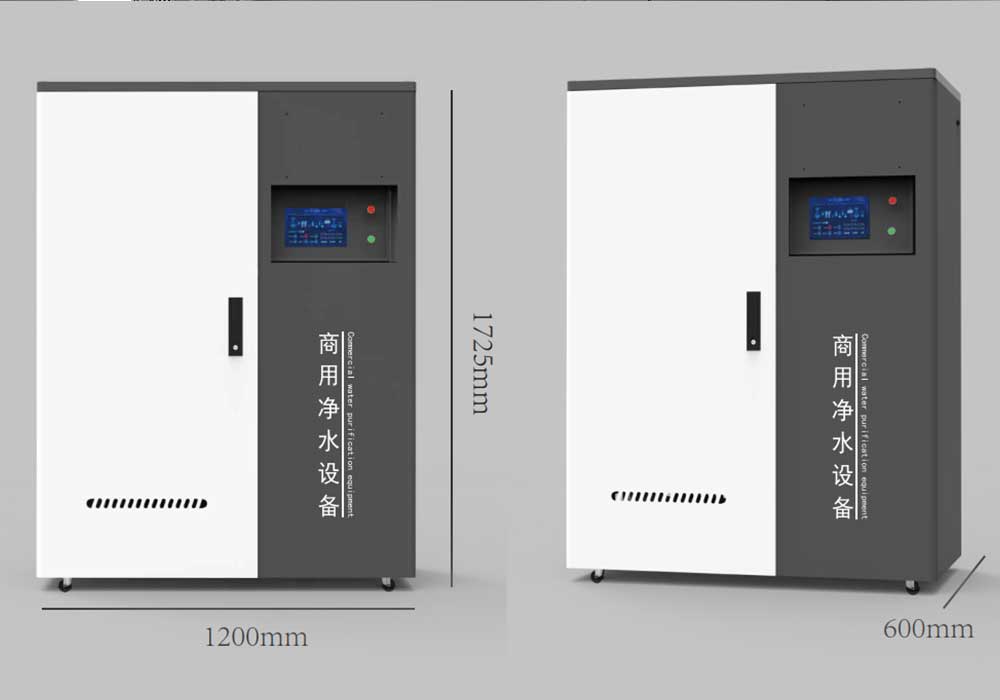
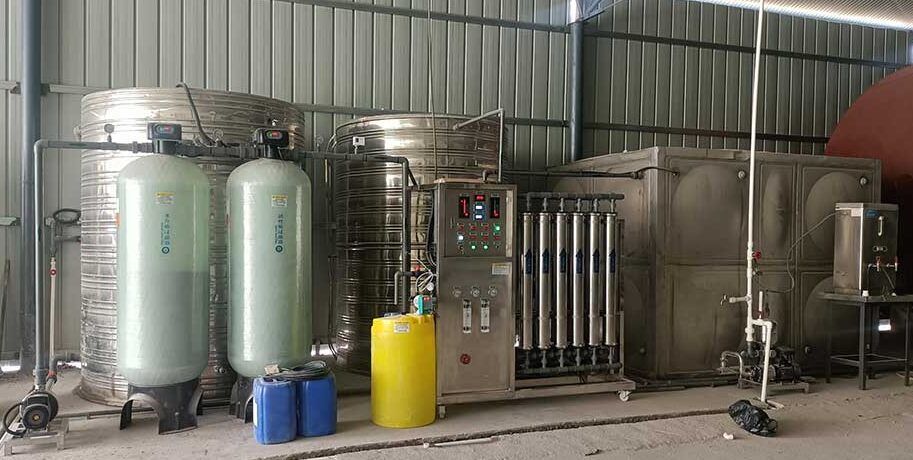
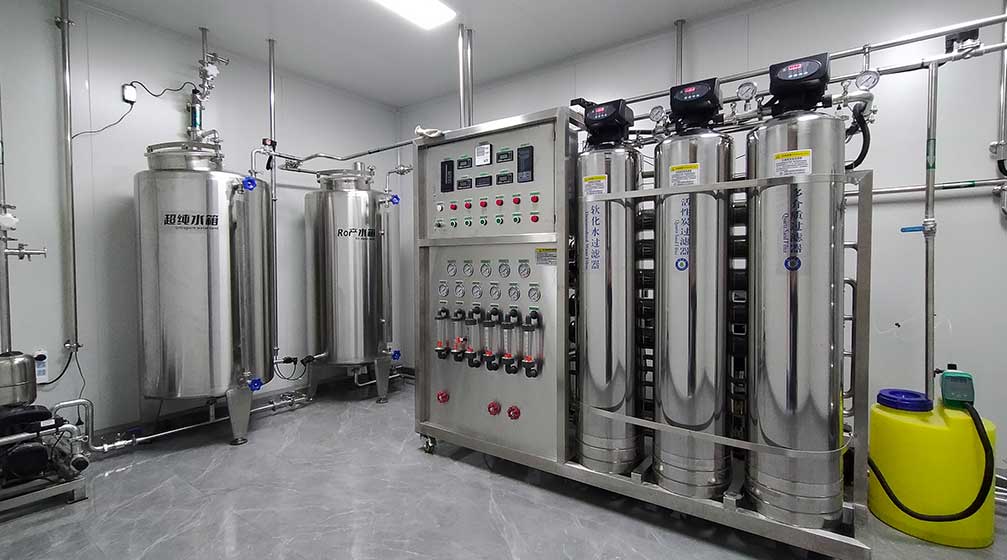
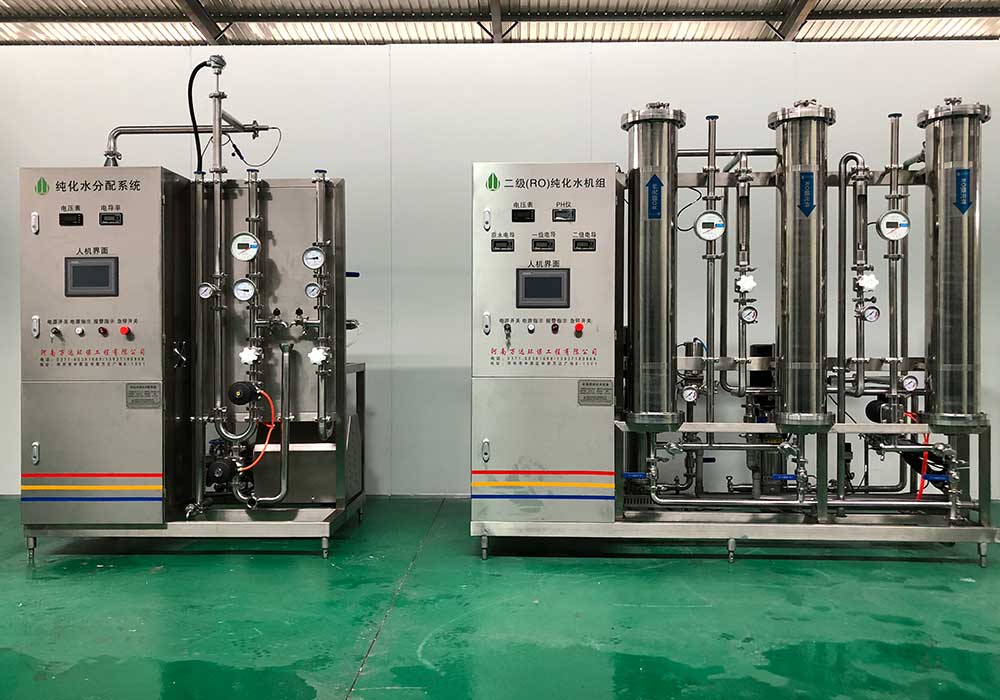
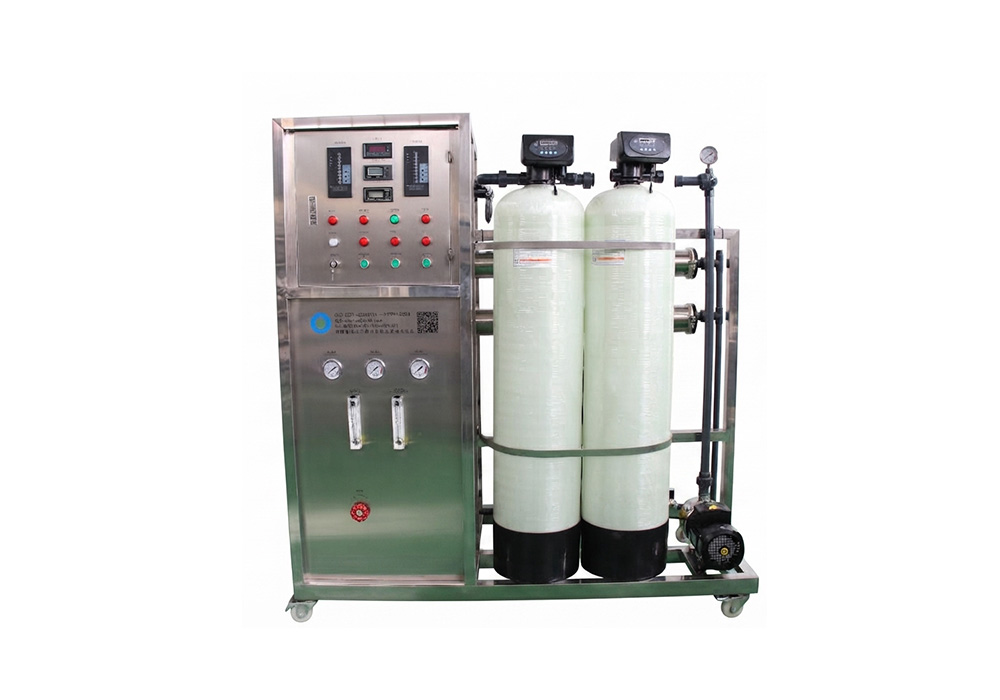
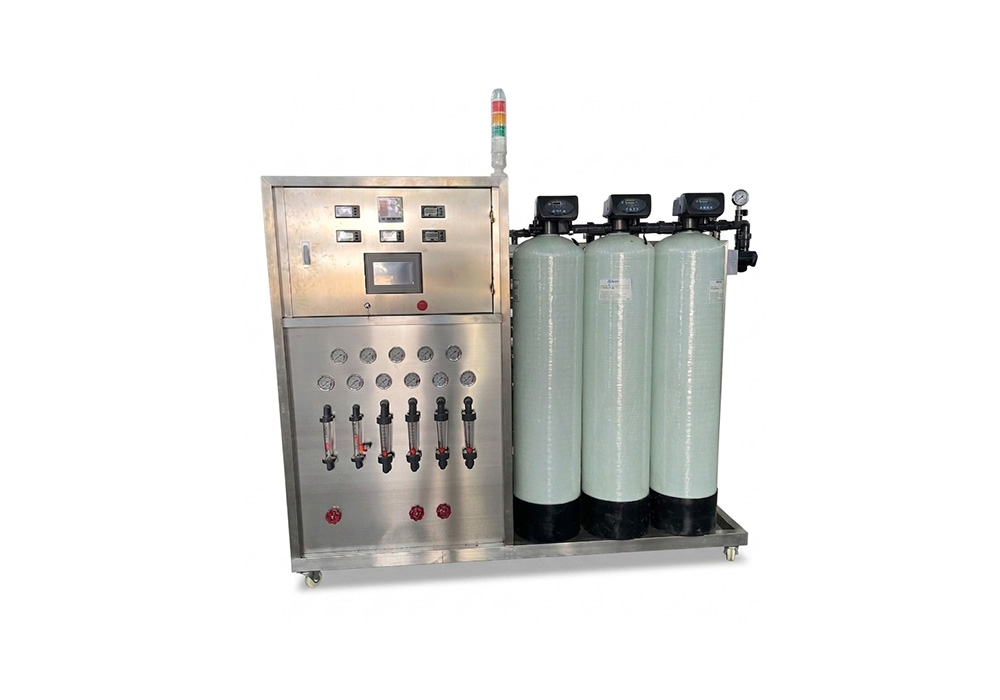
Reverse osmosis (RO) water treatment systems, as a highly efficient core technology for membrane separation and desalination, have given rise to a variety of application classifications covering tap water purification, brackish water and seawater desalination, and wastewater reuse. They support single-stage, double-stage, or RO+EDI ultra-pure water combination processes. Structurally, they can be flexibly selected as skid-mounted, containerized, or fully enclosed cabinet types. We comprehensively offer in-depth customization services based on production capacity scale, food-grade 304/316L materials, first-line brand components and intelligent PLC automation control, precisely meeting the strict high-purity water preparation requirements of industrial, commercial and high-end manufacturing fields.
Product Classification
Frequently Asked Questions (FAQ)
We employ a “consultative design” approach. We align deeply with your technical team during the design phase, delivering PFDs and 3D layouts to ensure the system perfectly matches your specific process constraints.
We establish a project baseline during the “Solution Finalization” phase. If adjustments are needed after the baseline is locked, we conduct an engineering impact assessment and provide a supplemental agreement, ensuring full transparency in project timelines and costs.
We adhere to a “transparency-first” principle. We provide a Bill of Materials (BOM) specifying the brand and model of all core components during the design phase, prioritizing Tier-1 global brands to ensure peak performance and global serviceability.
We adhere to rigorous quality management systems (ISO9001). For export projects, we support manufacturing compliant with international standards such as CE, UL, and ASME to meet your specific regional regulatory requirements.
For custom systems, we execute rigorous Factory Acceptance Testing (FAT). Protocols are tailor-made for your unique requirements, and we invite you to witness critical test stages via remote video. A comprehensive test report is included in the shipment.
Lead times depend on project scale and complexity. We clearly define key milestones—manufacturing, FAT, and shipping—in the contract to ensure transparent scheduling and timely project progression.
We provide 24/7 remote support via video guidance and online diagnostics. Senior engineers are available for on-site installation and commissioning services upon request.
We provide a comprehensive list of consumables upon delivery and offer full-lifecycle support. We ensure the regular supply of spare parts to prevent operational downtime.