Introduction: The Growing Demand for High-Purity Water
In the modern industrial landscape, water is more than just a utility; it is a critical raw material. From the microscopic cleansing of semiconductor wafers to the precise formulation of biopharmaceuticals, the requirement for water purity has reached unprecedented levels. As a professional manufacturer with over 20 years of experience, PureReach is witnessing a global shift toward integrated Reverse Osmosis (RO) and Electrodeionization (EDI) systems as the gold standard for high-performance production.
I. The Synergy of RO and EDI: Beyond Traditional Filtration
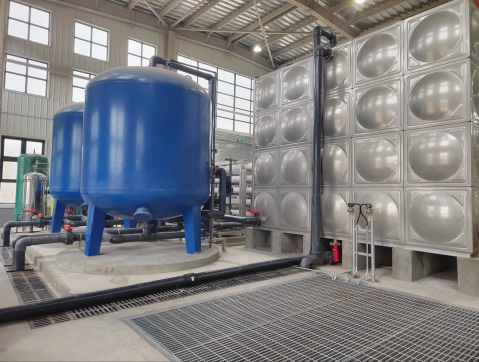
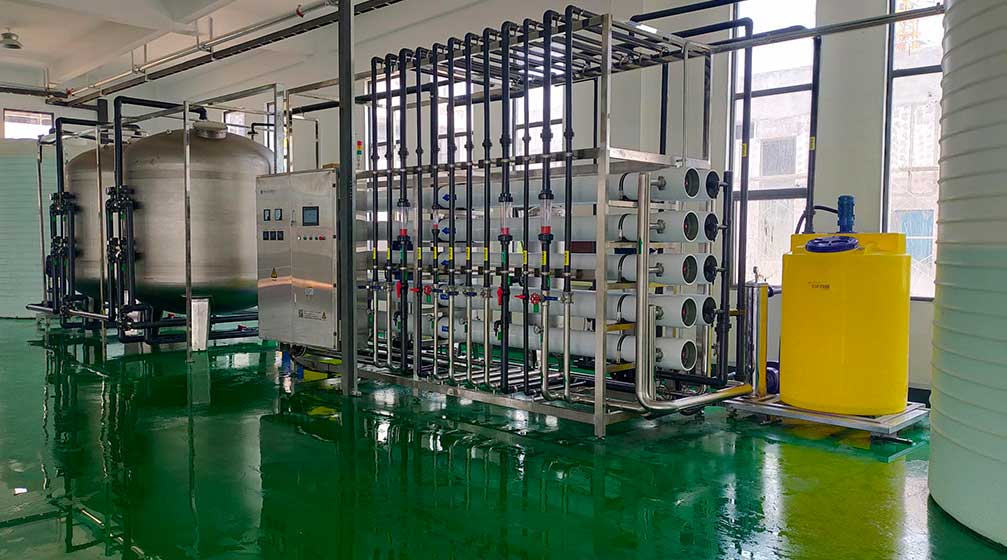
Traditional ion-exchange methods, while effective, involve significant downtime and the handling of hazardous chemicals. The integration of RO and EDI technologies creates a seamless, continuous purification loop:
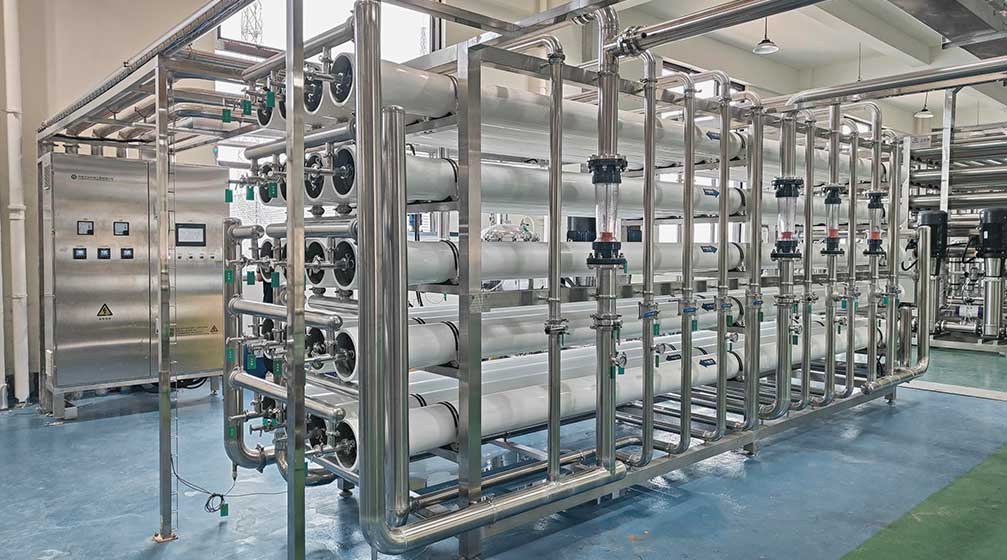
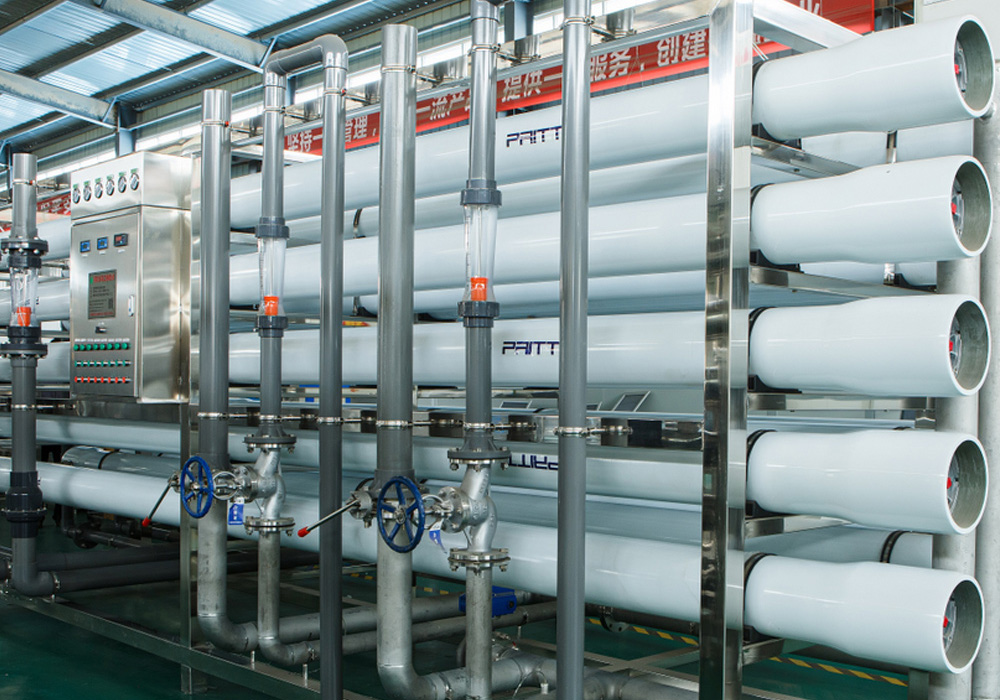
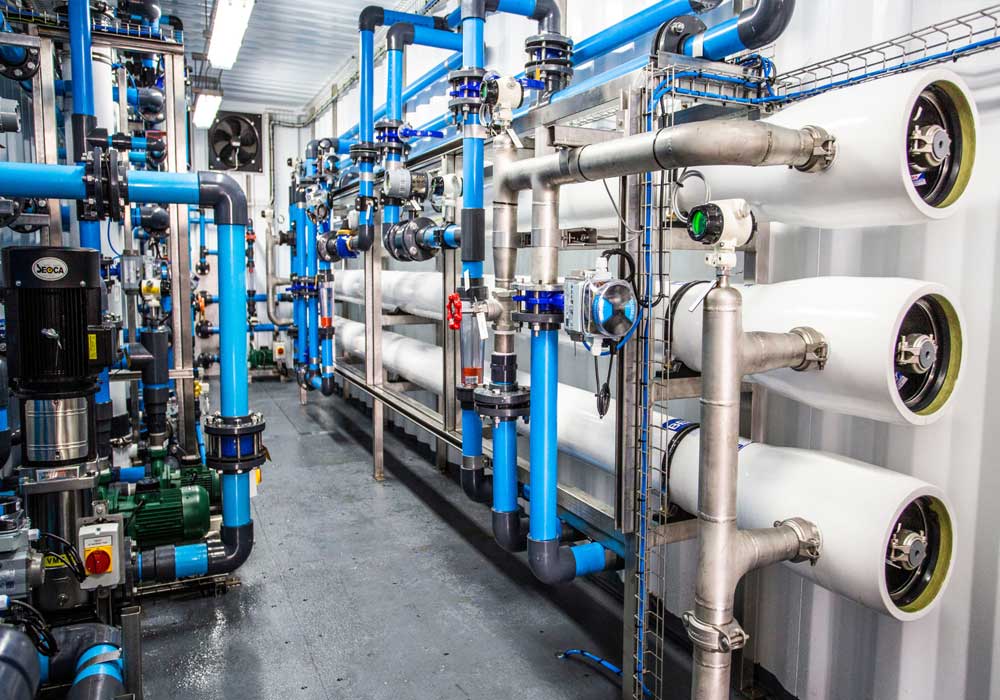
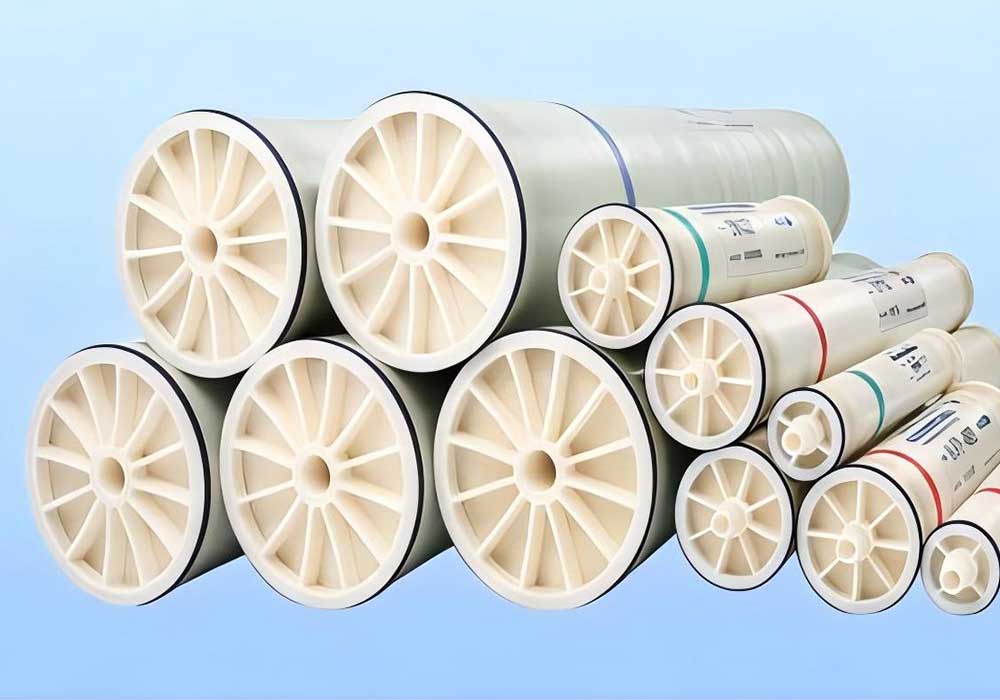
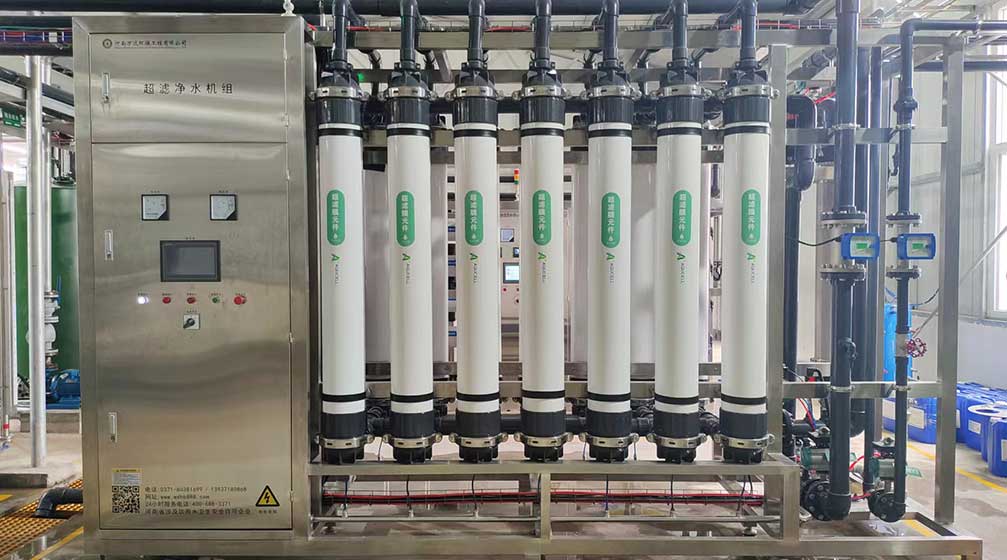
- Dual-Stage RO Pre-treatmentOur advanced RO membranes remove up to 99.5% of dissolved salts and organic contaminants, shielding the delicate EDI modules from scaling.
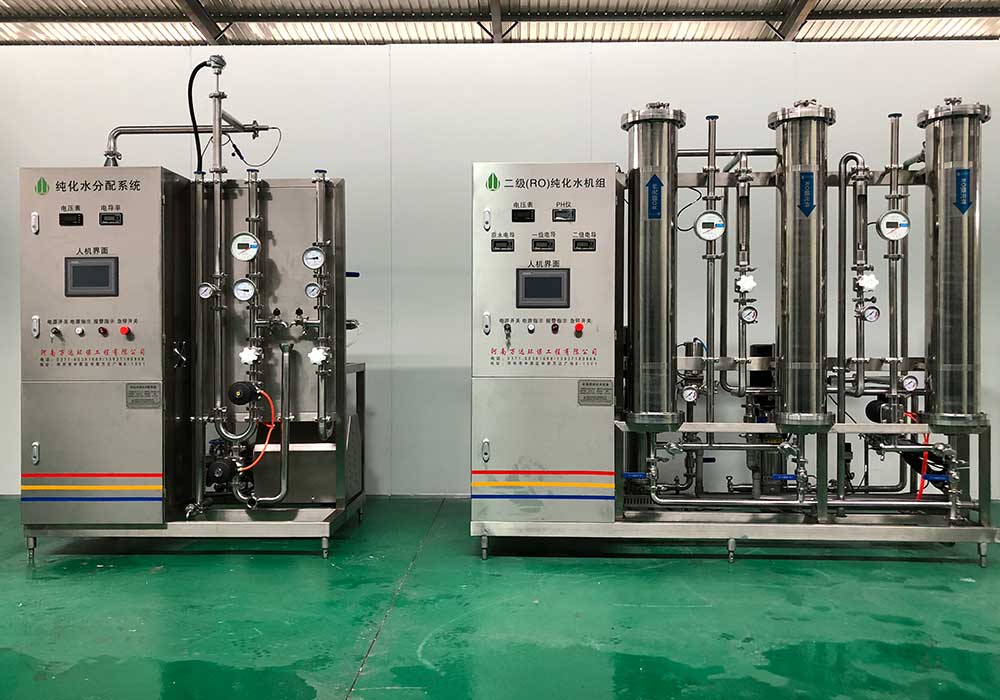
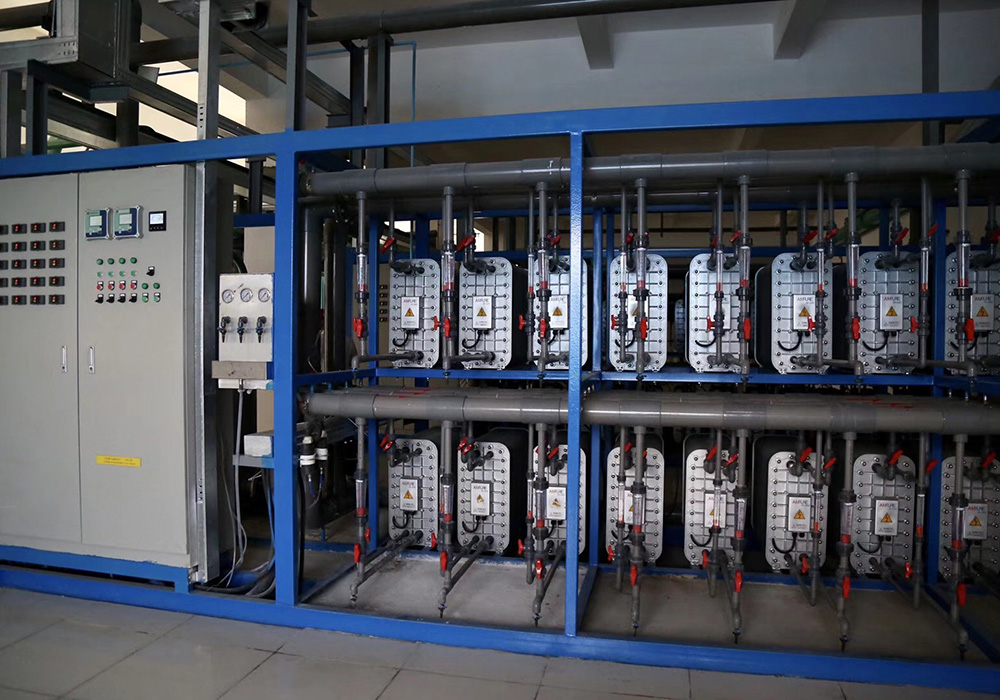
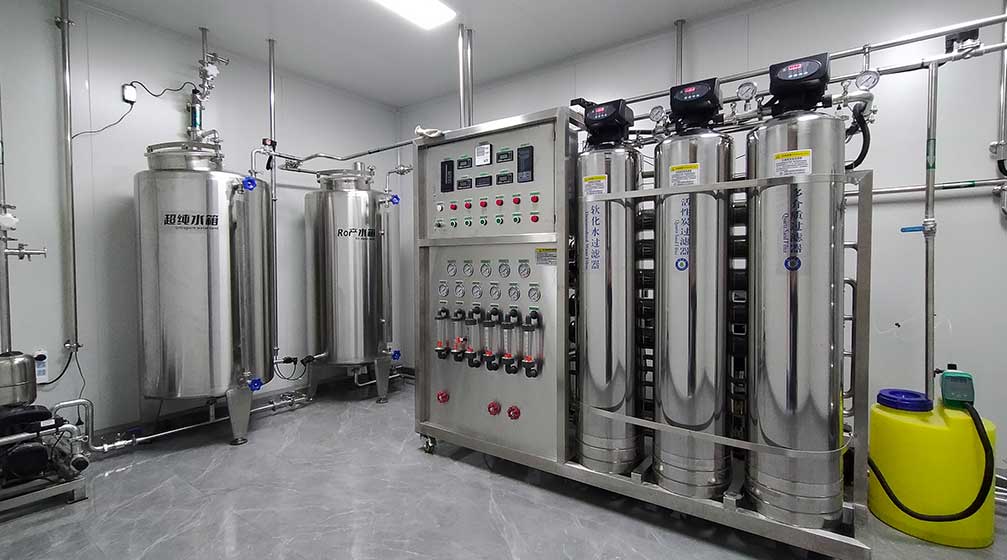
- Continuous EDI Polishing By utilizing electrical current instead of acids or alkalis, our EDI systems achieve a stable output of 18.2 MΩ·cm, meeting the most stringent USP and ASTM standards.
- Continuous EDI Polishing By utilizing electrical current instead of acids or alkalis, our EDI systems achieve a stable output of 18.2 MΩ·cm, meeting the most stringent USP and ASTM standards.
II. Engineering for Complex Feedwater: The PureReach Approach
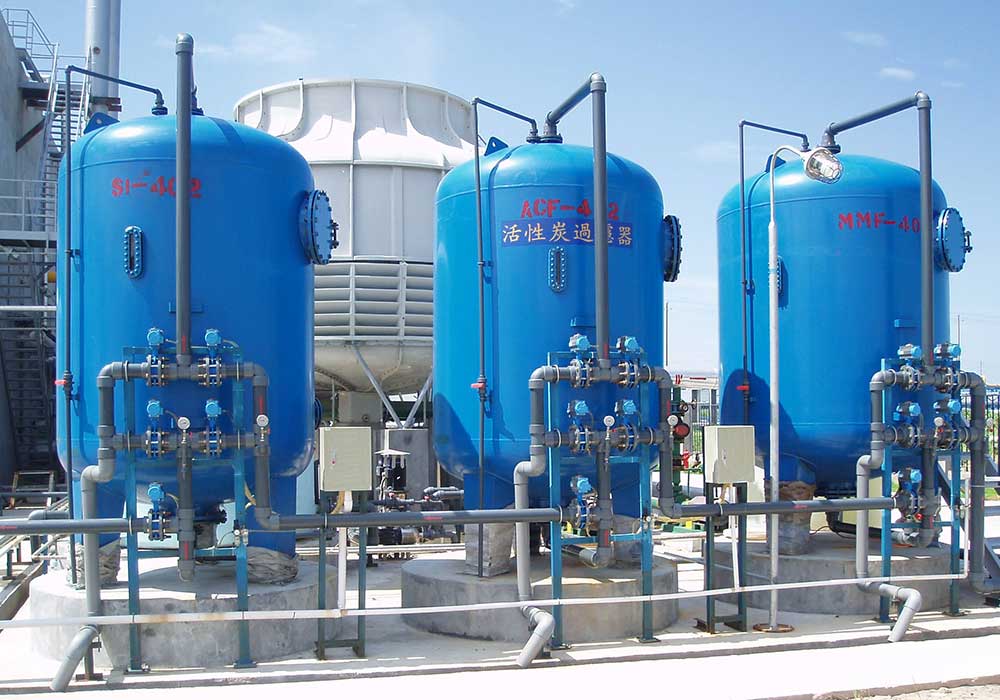
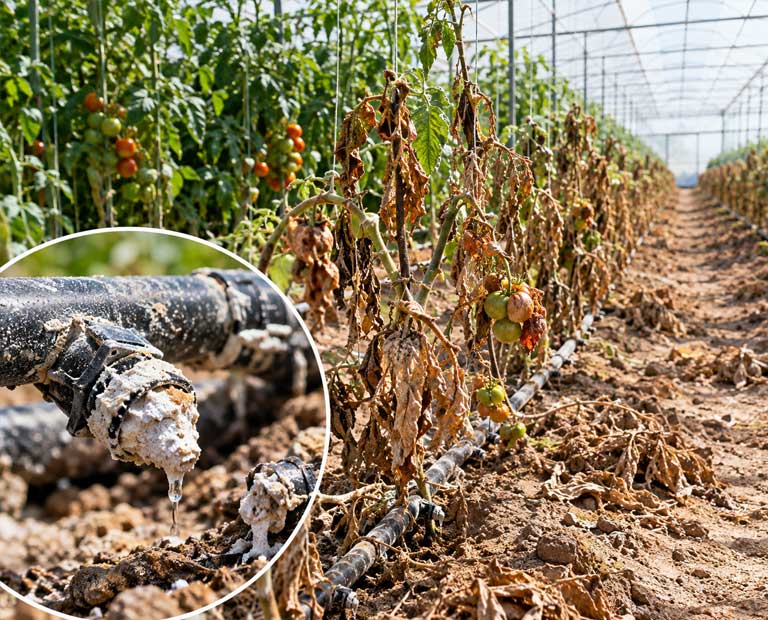
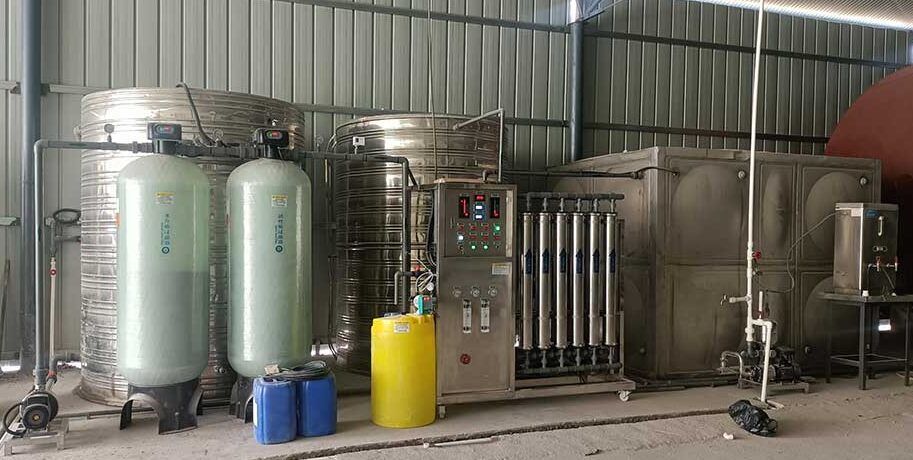
No two industrial sites have the same raw water chemistry. Our engineering team specializes in Customized Solutions tailored to diverse feedwater conditions. For heavy industries like metallurgy and chemical processing, we implement specialized anti-fouling membranes and smart dosing systems. This precision engineering ensures that even in regions with high-hardness or high-salinity water, our systems maintain peak flux and long-term membrane integrity.
III. Sustainability as a Competitive Advantage
In 2026, “Green Manufacturing” is no longer just a buzzword PureReach’s integrated systems focus on two critical eco-metrics:
- Chemical-Free Operation EDI eliminates the need for onsite chemical storage and neutralisation tanks, reducing the factory’s environmental footprint.
- High Water Recovery Through multi-stage recovery arrays, we help clients achieve up to 90% system recovery, significantly lowering the cost per ton of ultrapure water and supporting global “Zero Liquid Discharge” (ZLD) initiatives.
IV. Smart Monitoring & Global Reach
The future of water treatment lies in connectivity. Our latest systems are equipped with IoT-enabled sensors that provide real-time data on conductivity, flow rates, and pressure differentials. This “Digital Twin” capability allows PureReach engineers to provide remote diagnostic support to our partners worldwide—from the Middle East to South America—ensuring that “Pure Water, Global Reach” is backed by reliable technical oversight.
Conclusion: Partnering for a Purer Future
As we look toward the next decade, PureReach remains committed to creating real value for manufacturers. By combining 20 years of technical rigor with a forward-looking commitment to sustainability, we provide more than just equipment; we provide the foundation for industrial excellence.